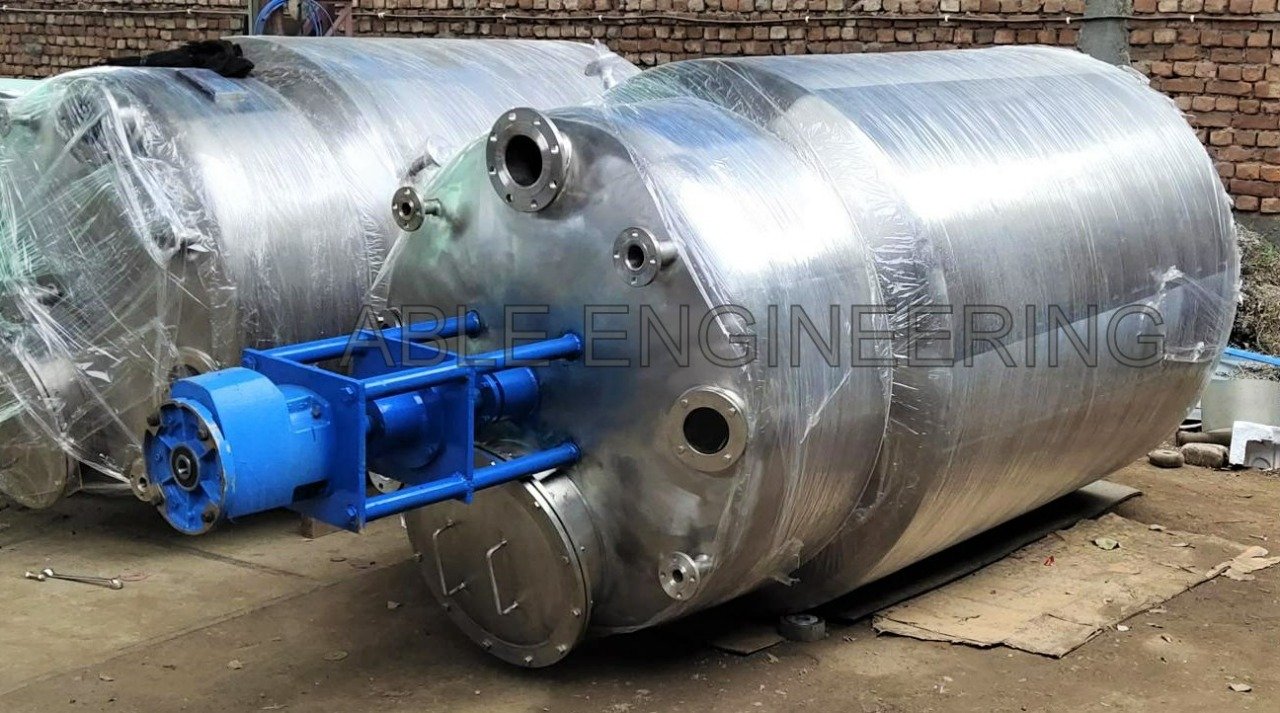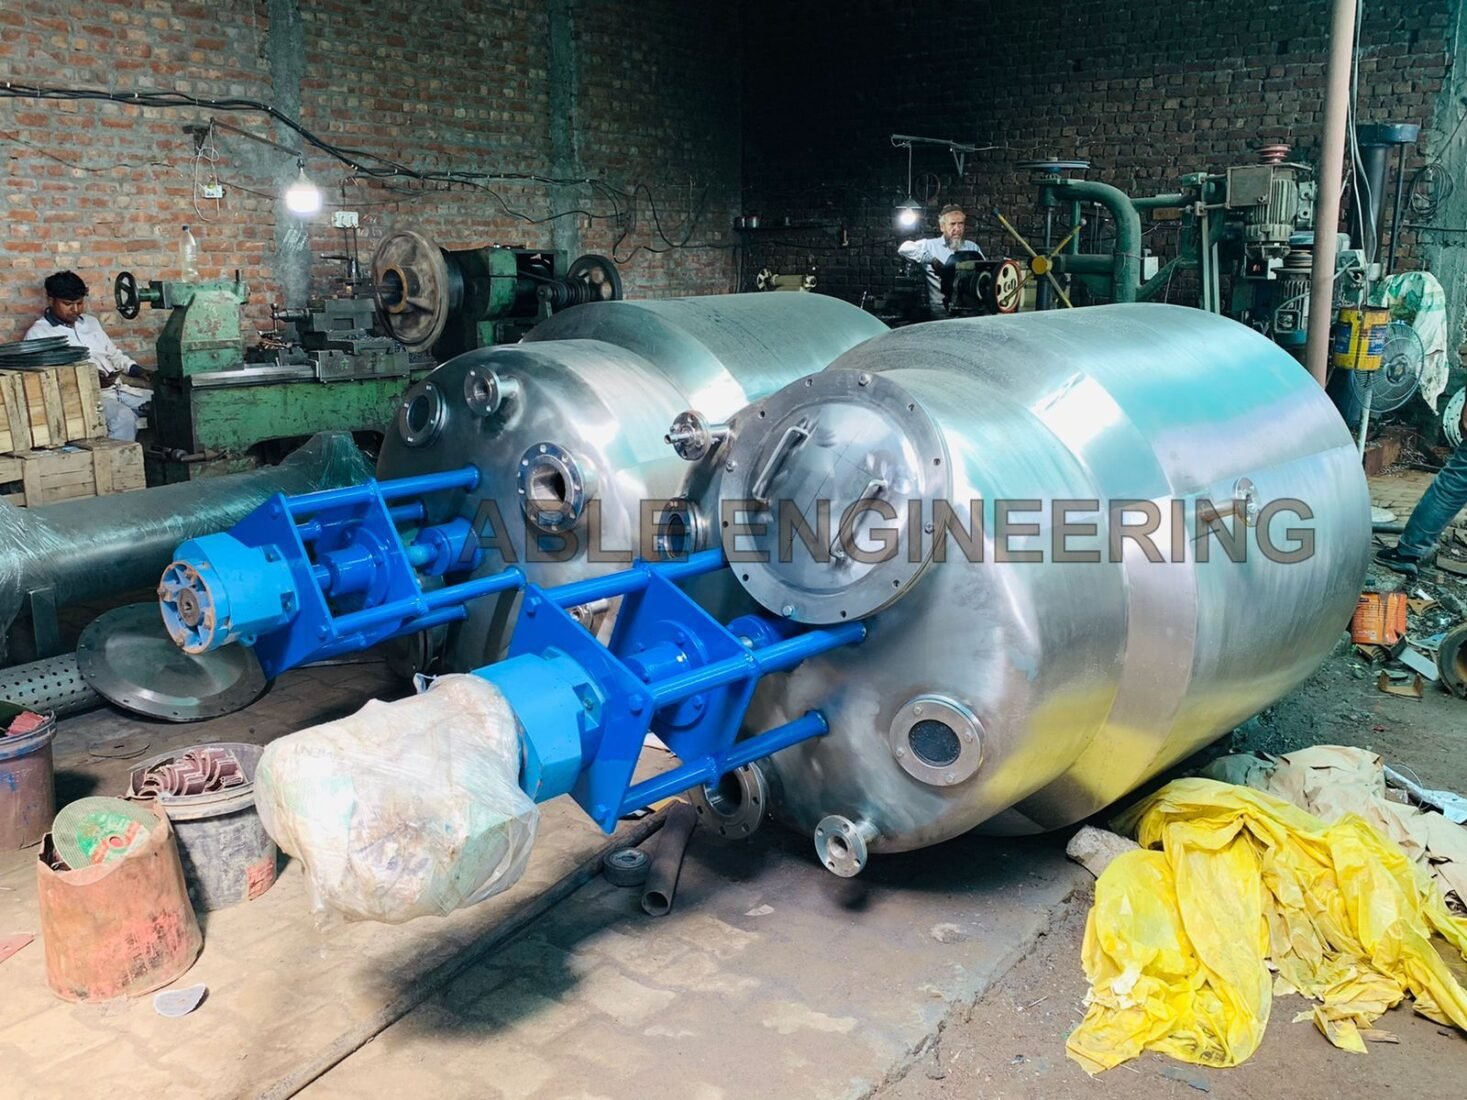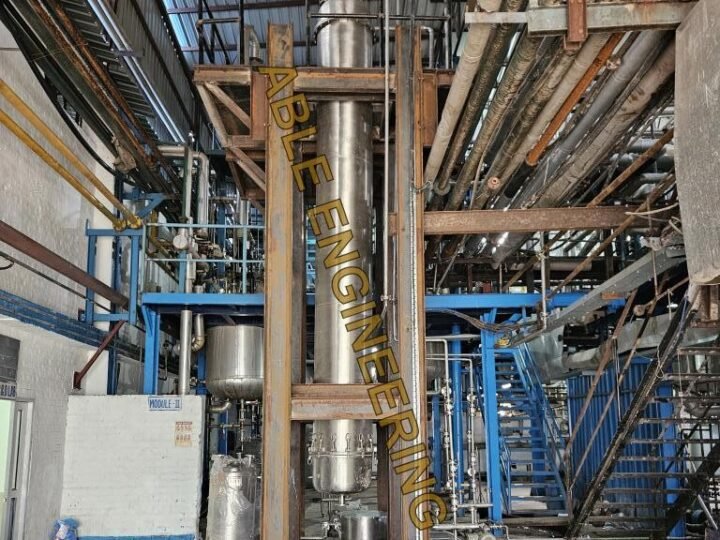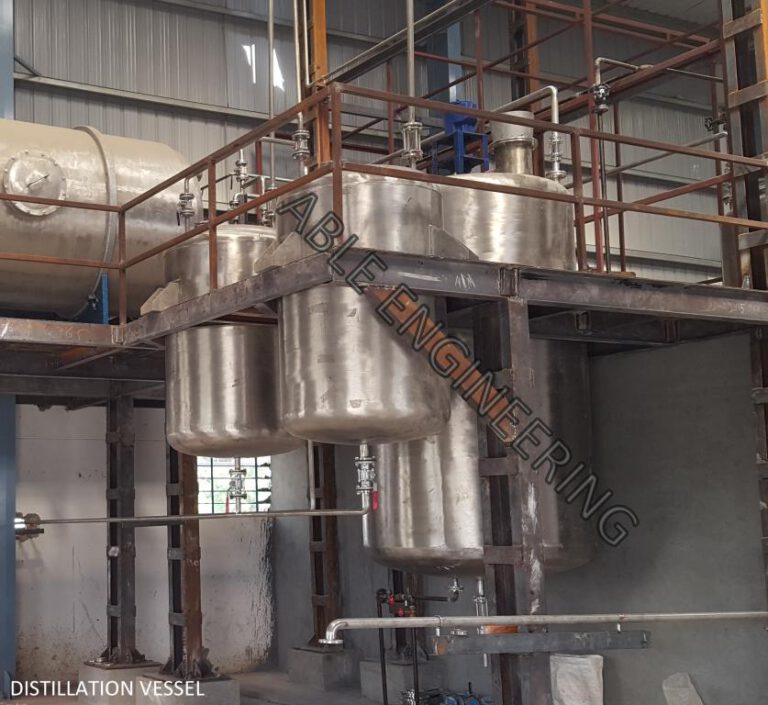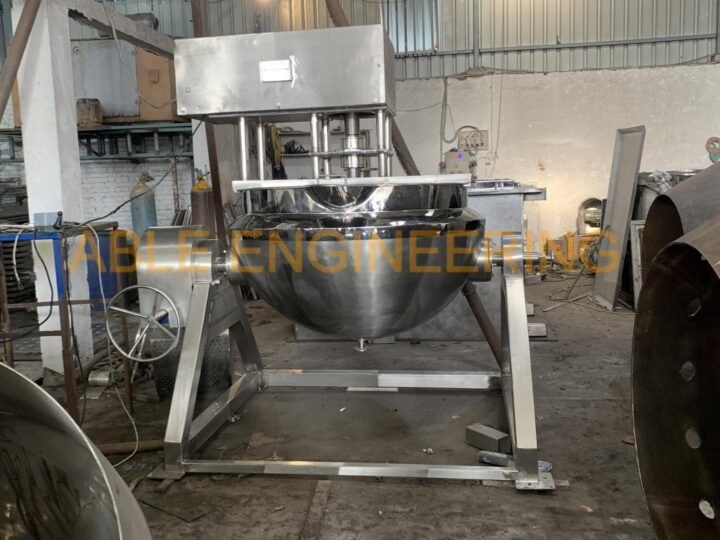
Reaction Vessel
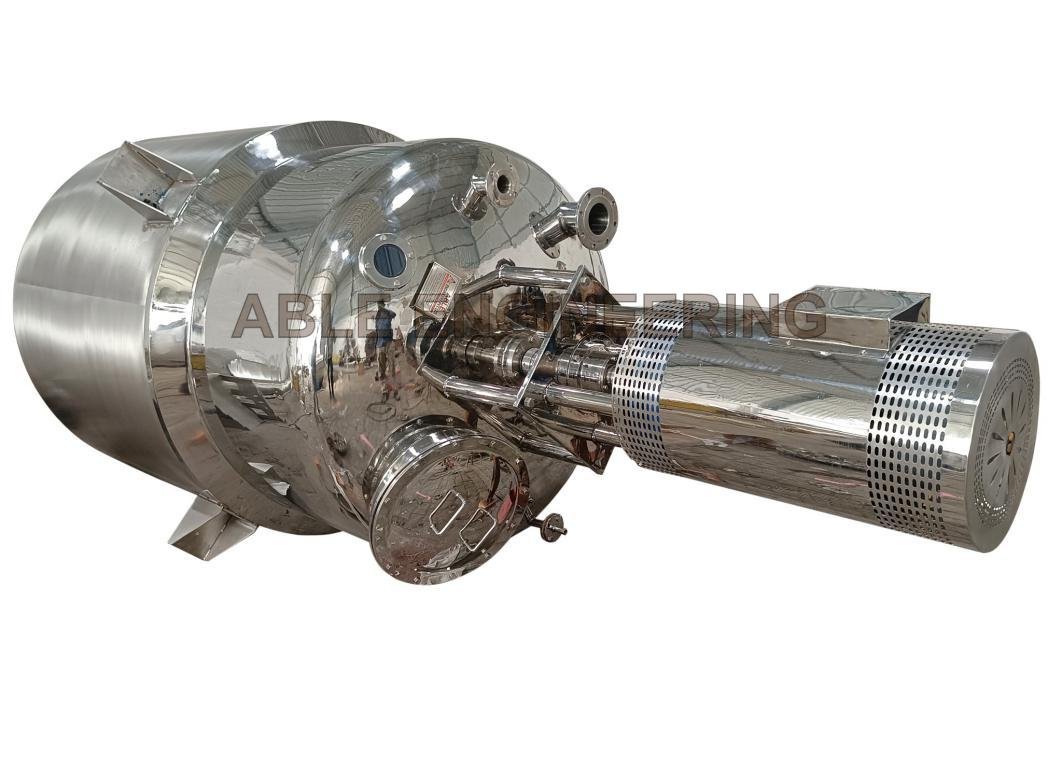
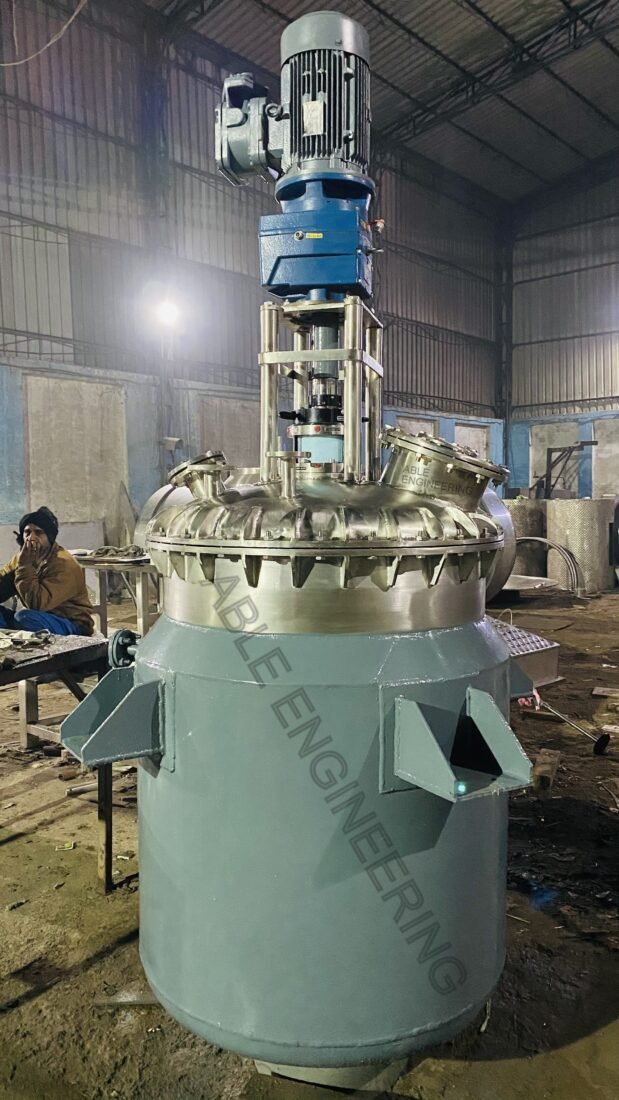
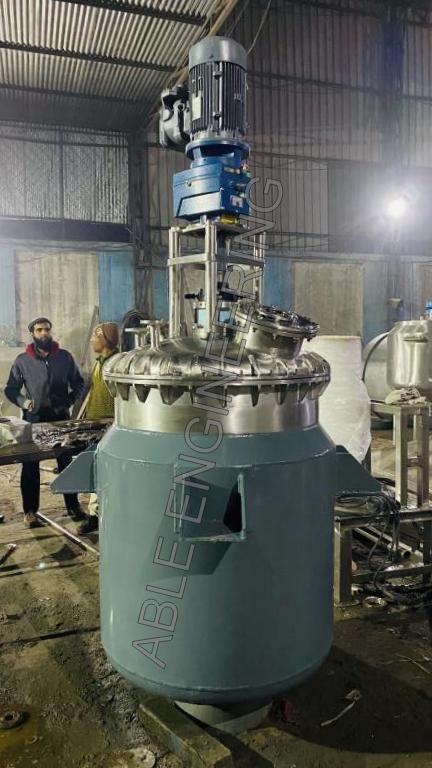
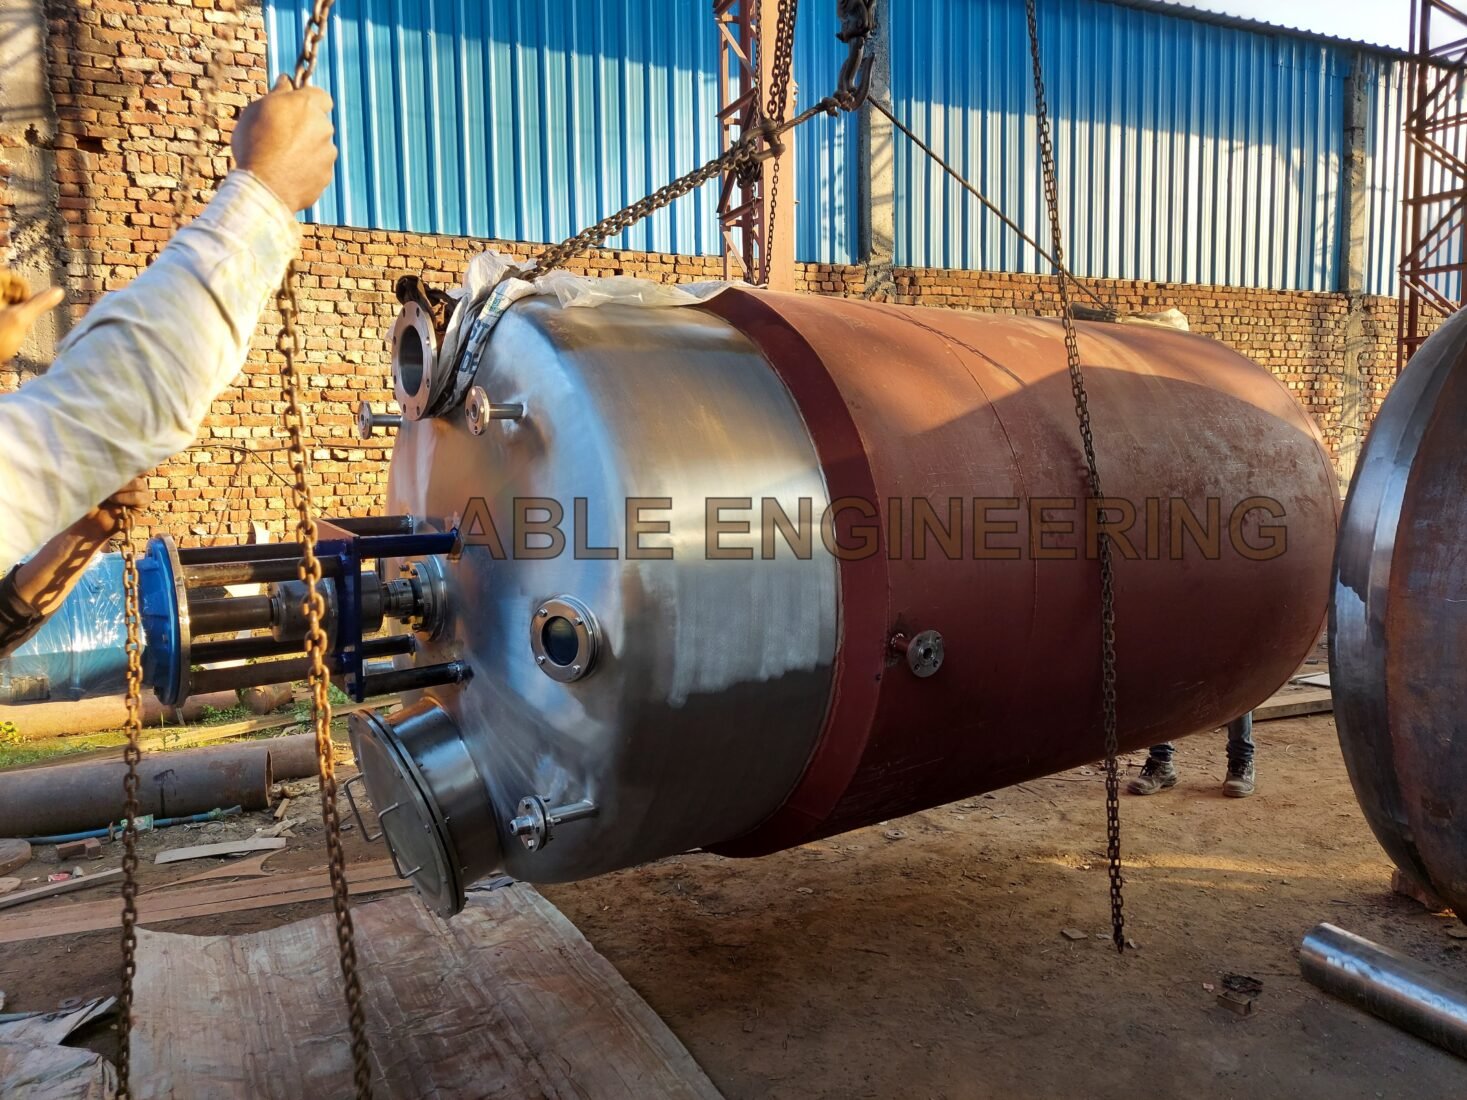
Reaction vessel is used in Herbal Extraction Plant and chemical plants for any chemical changes and processes of reaction.

Built around your process.
A Reaction Vessel is industrial equipment that enables chemical changes and reactions in Herbal Extraction Plants, Pharmaceutical Plants, and Chemical Plants. It provides a controlled environment for chemical processing and plays a vital role in industrial production.
In fact, Reaction Vessels form the heart of a Chemical Plant because they support a wide range of chemical processes. These include Condensation, Polymerization, Esterification, Etherification, Hydrolysis, Hydration, Reduction, Oxidation, and Hydrogenation. Depending on the process, each reaction requires specific operating conditions and equipment configurations.
For construction, industries commonly use Stainless Steel, Glass-Lined Steel, Glass, or Ceramics. The selection depends on chemical compatibility and process requirements. Moreover, different agitators ensure effective mixing and help achieve the desired process results. Common options include Anchor Type, Propeller Type, Paddle Type, and Pitched-Blade Turbine Type Agitators. For intensive mixing, we can also incorporate a High-Speed Homogenizer according to the application.
Our Reaction Vessels generally range from 500 Litres to 25,000 Litres in capacity. However, we also customize the capacity, construction material, and agitator configuration to meet specific production requirements.
Able Engineers Private Limited manufactures efficient and durable Reaction Vessels using quality materials and suitable engineering designs. Furthermore, we offer a wide range of customized solutions at competitive prices to meet diverse industrial requirements.
Features of Reaction Vessel
- Handles a wide range of Chemical Reactions and industrial processes
- Serves Herbal Extraction Plants, Pharmaceutical Plants, and Chemical Plants
- Offers Stainless Steel, Glass-Lined Steel, Glass, and Ceramic construction options
- Supports different agitator configurations for effective mixing
- Includes Anchor, Propeller, Paddle, and Pitched-Blade Turbine Agitators
- Accommodates a High-Speed Homogenizer for intensive mixing requirements
- Provides capacities from 500 Litres to 25,000 Litres
- Allows customization according to process conditions and client specifications
- Supports efficient operation and long-term industrial use
Applications of Reaction Vessel
Reaction Vessels serve various industries that require controlled chemical reactions, processing, and mixing.
- Herbal Extraction Industry: Facilitates chemical reactions and processing during herbal extraction.
- Pharmaceutical Industry: Supports chemical reactions involved in pharmaceutical manufacturing.
- Chemical Industry: Handles Condensation, Polymerization, Esterification, Etherification, Hydrolysis, Hydration, Reduction, Oxidation, and Hydrogenation.
- Nutraceutical Industry: Supports chemical processing and reactions involving nutraceutical ingredients.
- Ayurvedic Industry: Facilitates processing and reaction requirements in Ayurvedic manufacturing.
- Food Processing Industry: Serves suitable reaction-based and industrial mixing applications.
Technical Specifications
| Parameter | Specification |
|---|---|
| Equipment | Reaction Vessel |
| Capacity | 500 Litres to 25,000 Litres |
| Material of Construction | Stainless Steel, Glass-Lined Steel, Glass, or Ceramics |
| Agitator Types | Anchor, Propeller, Paddle, Pitched-Blade Turbine |
| Mixing Option | High-Speed Homogenizer |
| Applications | Chemical Reactions and Process Mixing |
| Reaction Types | Condensation, Polymerization, Esterification, Etherification, Hydrolysis, Hydration, Reduction, Oxidation, Hydrogenation |
| Design | Customized as per process requirements |
| Industries | Herbal, Pharmaceutical, Chemical, Nutraceutical, Ayurvedic, and Food Processing |
Note: We customize capacity, material of construction, agitator type, and other technical specifications according to client requirements.
Advantages of Reaction Vessel
- Versatile Applications: Handles different chemical reactions across multiple industries.
- Efficient Mixing: Offers suitable agitator configurations to meet specific process requirements.
- Material Flexibility: Provides multiple construction materials for different chemical applications.
- Customized Capacity: Accommodates diverse production requirements through flexible capacity options.
- Durable Construction: Uses quality materials and engineering for reliable industrial performance.
- Process Adaptability: Supports different chemical processing conditions and applications.
Reaction Vessel Manufacturer in India
Able Engineers Private Limited manufactures and supplies Reaction Vessels in India for various industrial applications. In addition, we manufacture Herbal Extraction Plants, Chemical Plants, and Herbal Extraction Plant Machinery.
We customize Reaction Vessels according to specific process requirements, including capacity, construction material, and agitator configuration. Moreover, we serve Herbal Extraction, Pharmaceutical, Chemical, Nutraceutical, Ayurvedic, and Food Processing Industries.
Contact us to discuss your industrial requirements and find a suitable Reaction Vessel for your process.