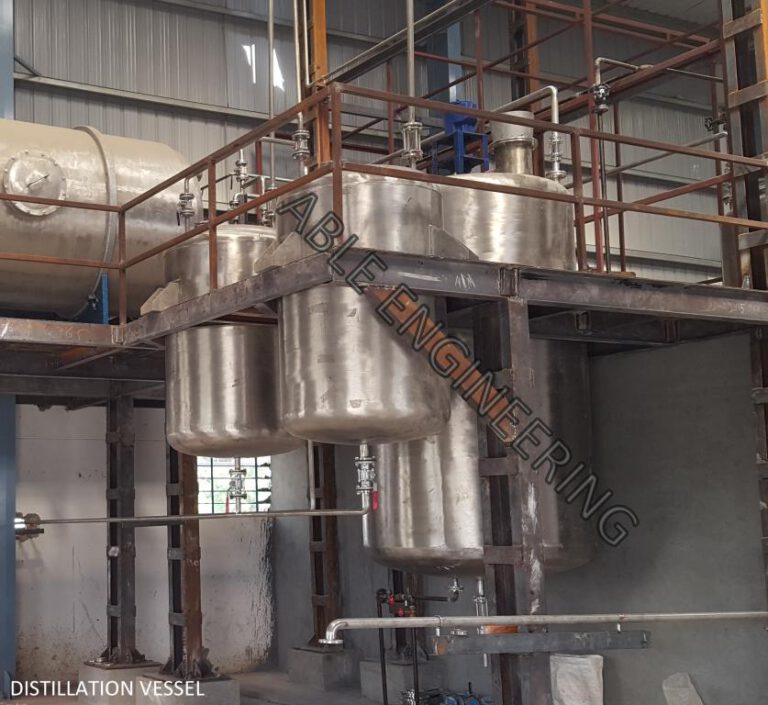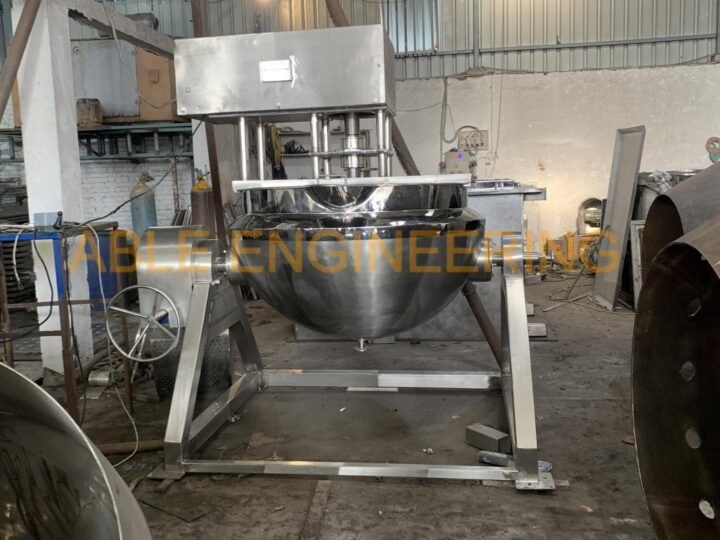
Chemical Reactor
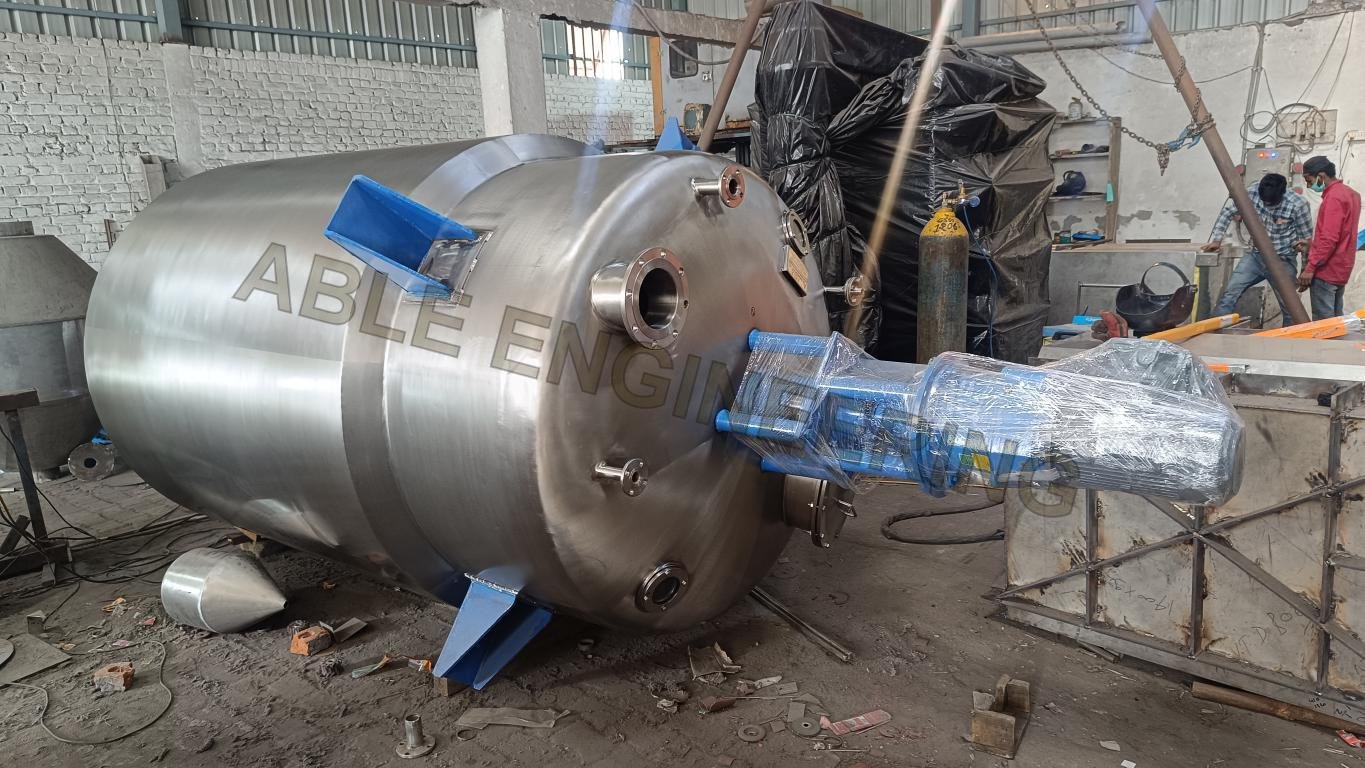
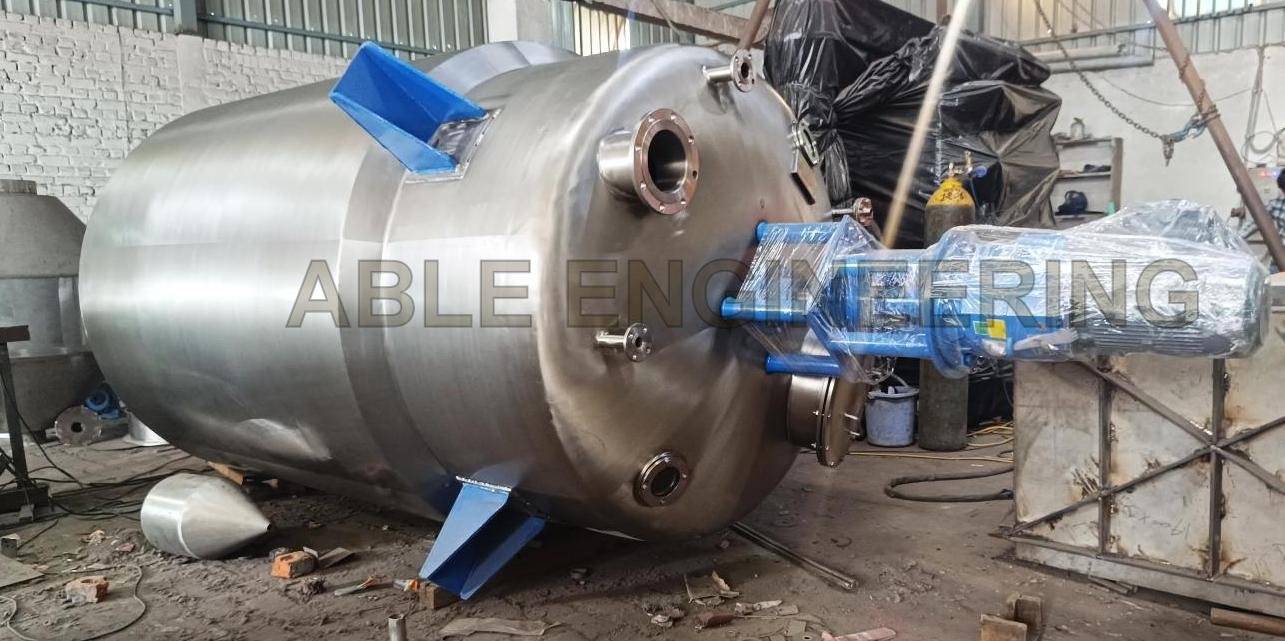
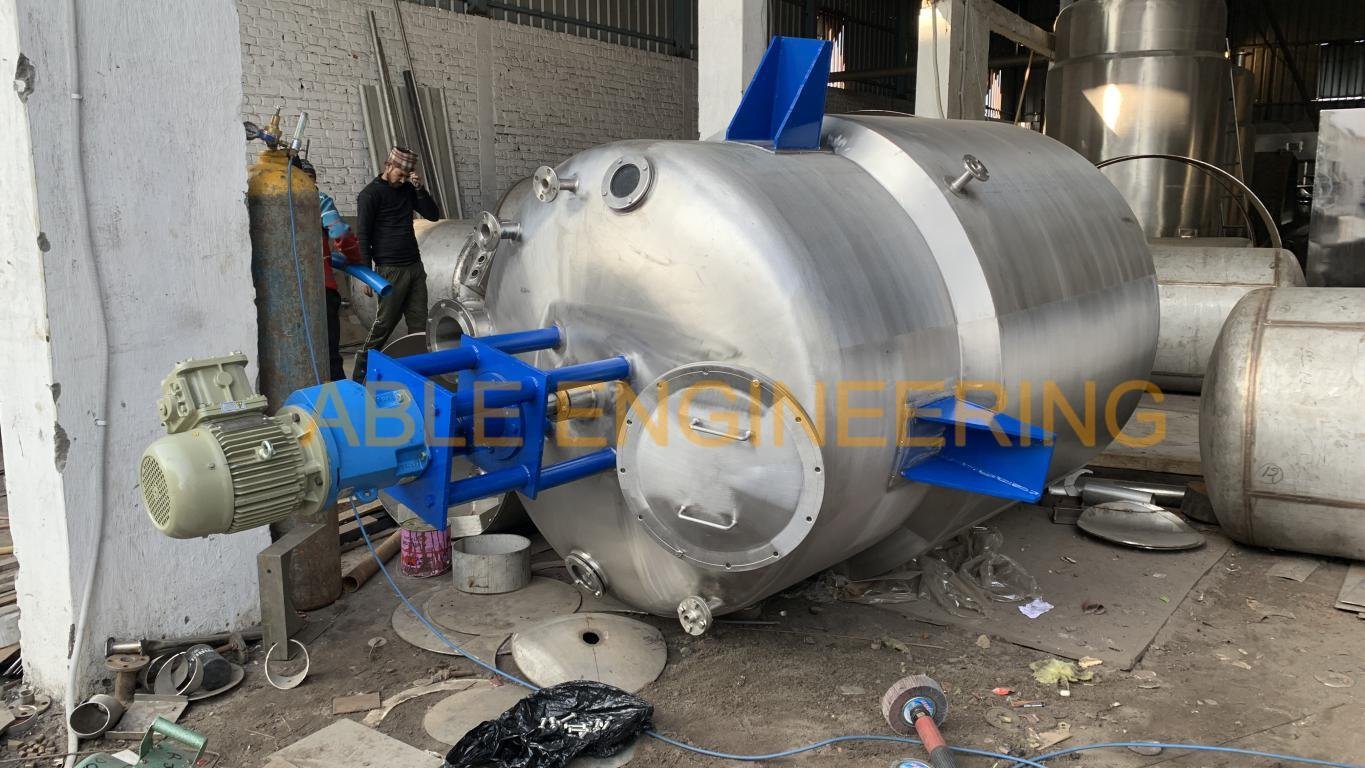
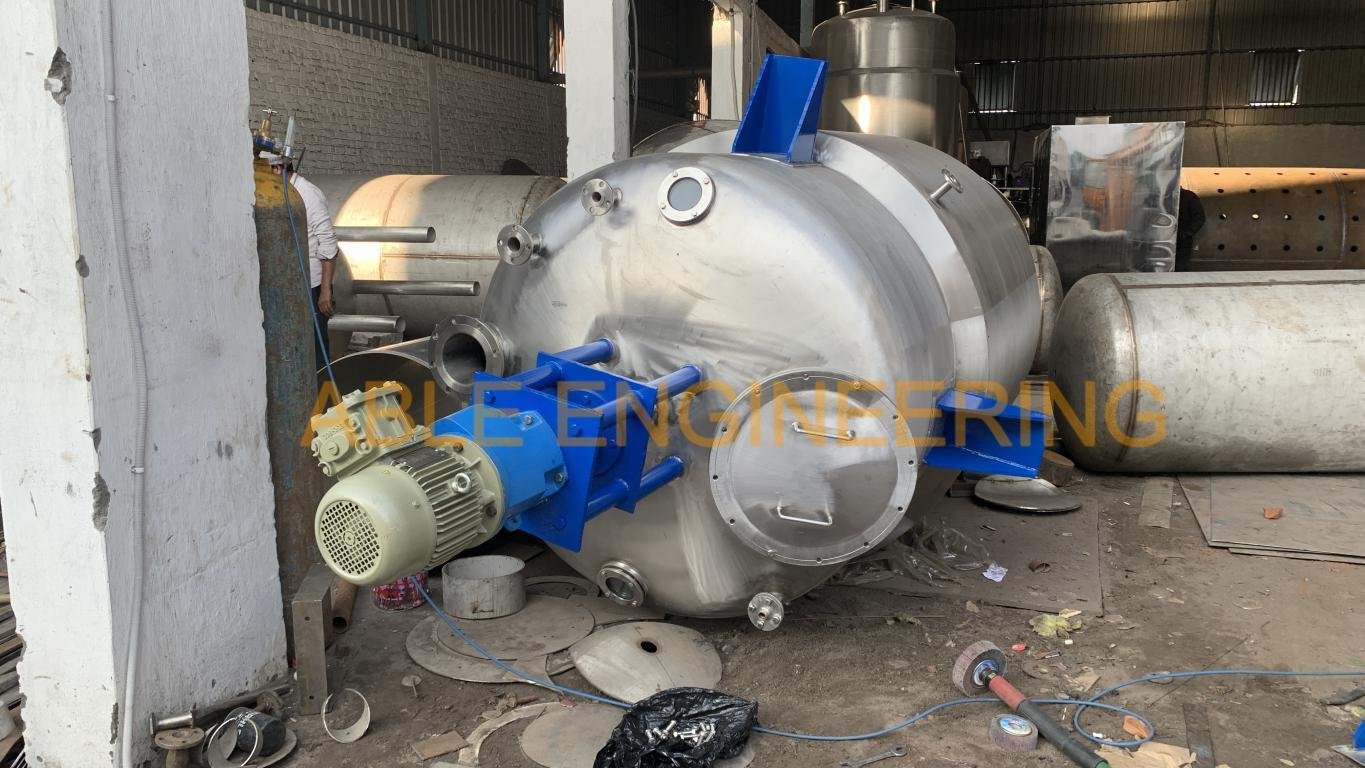
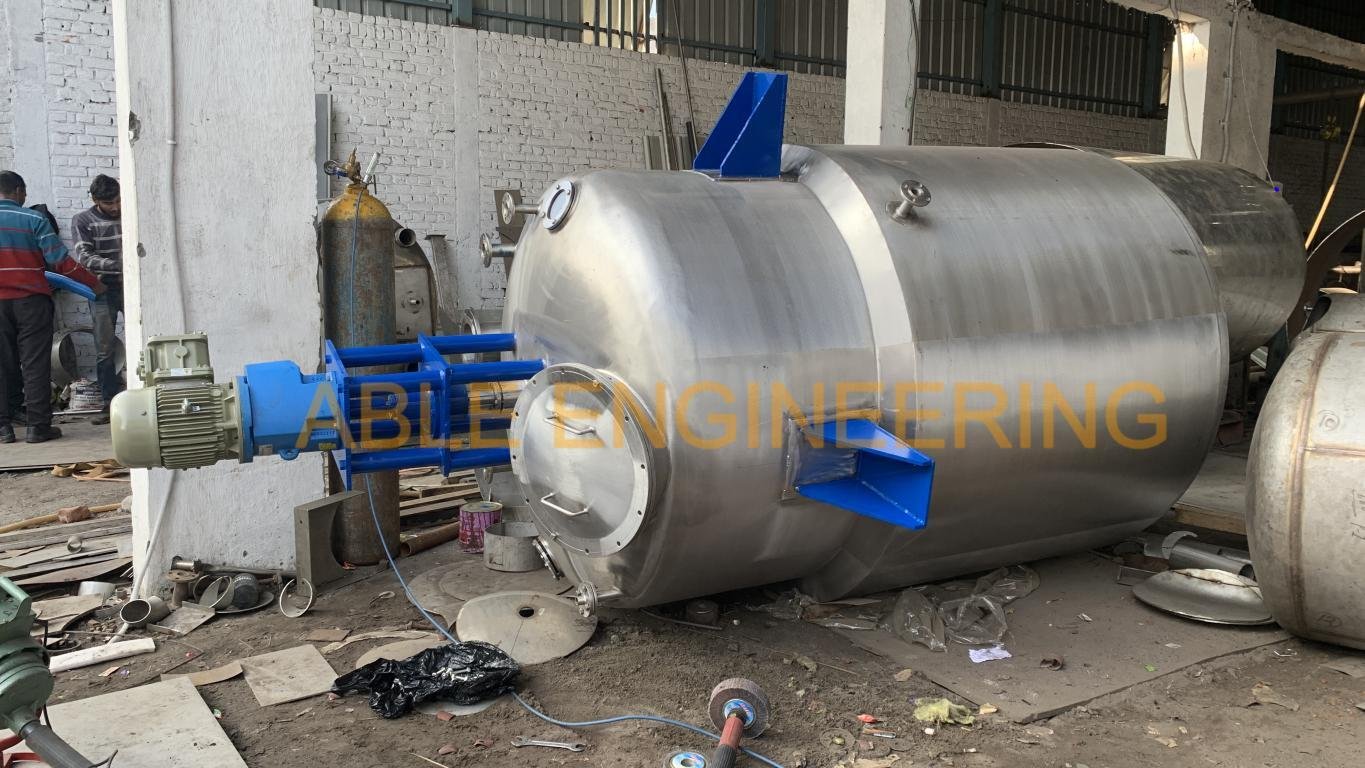
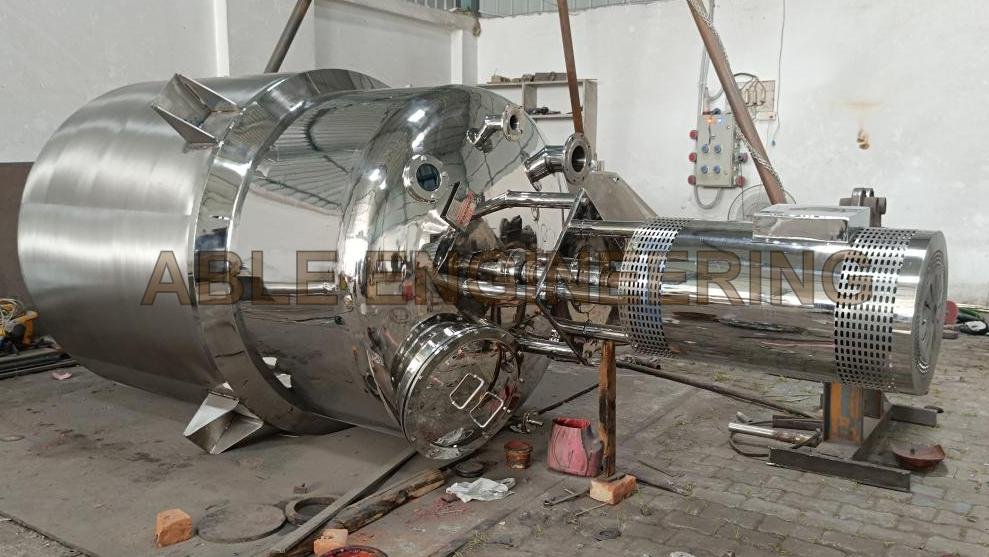
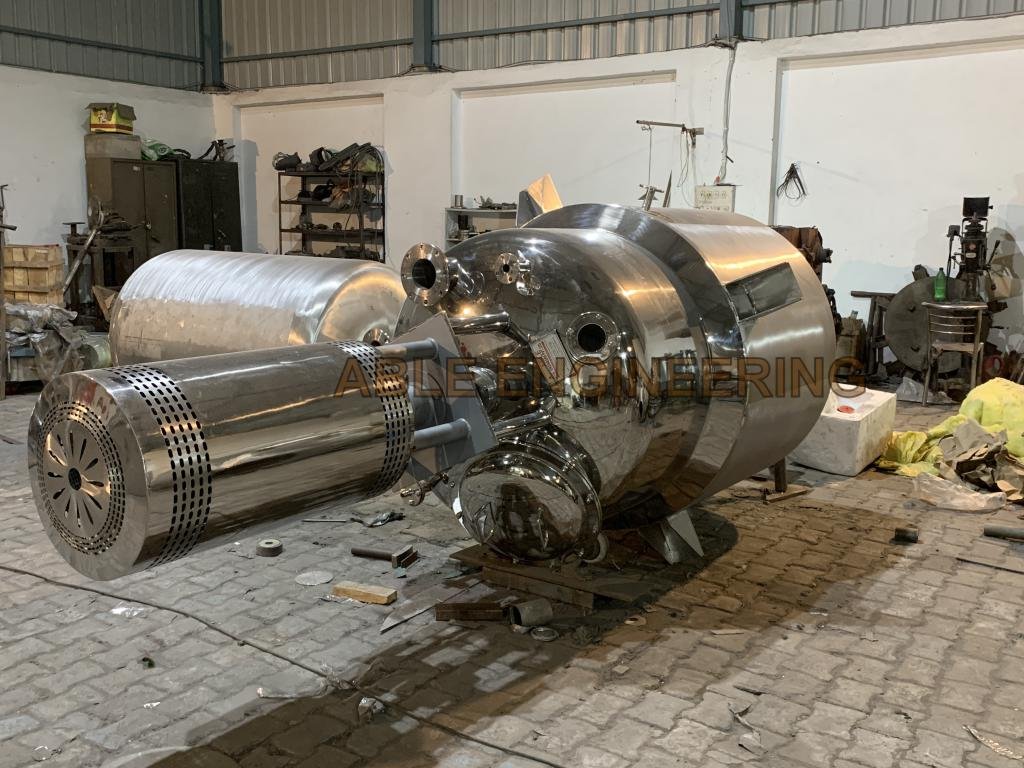
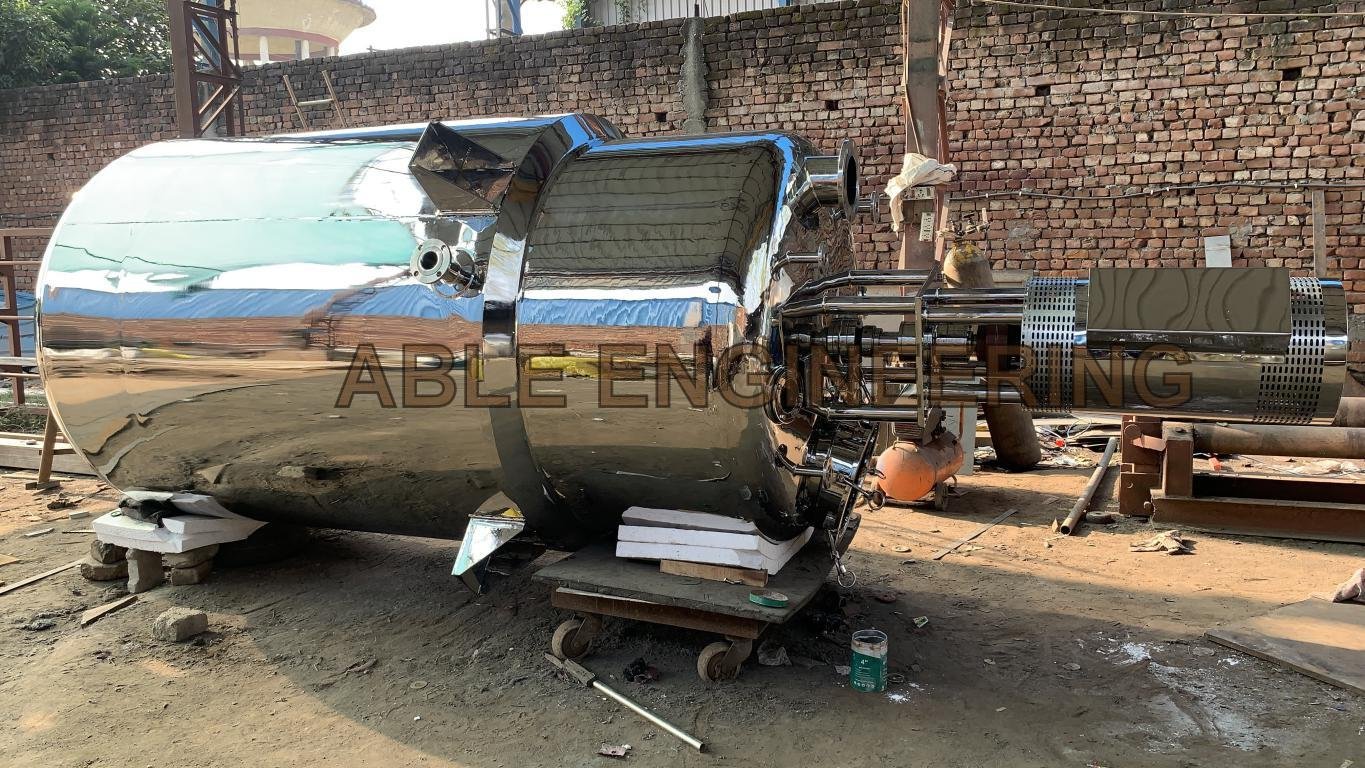
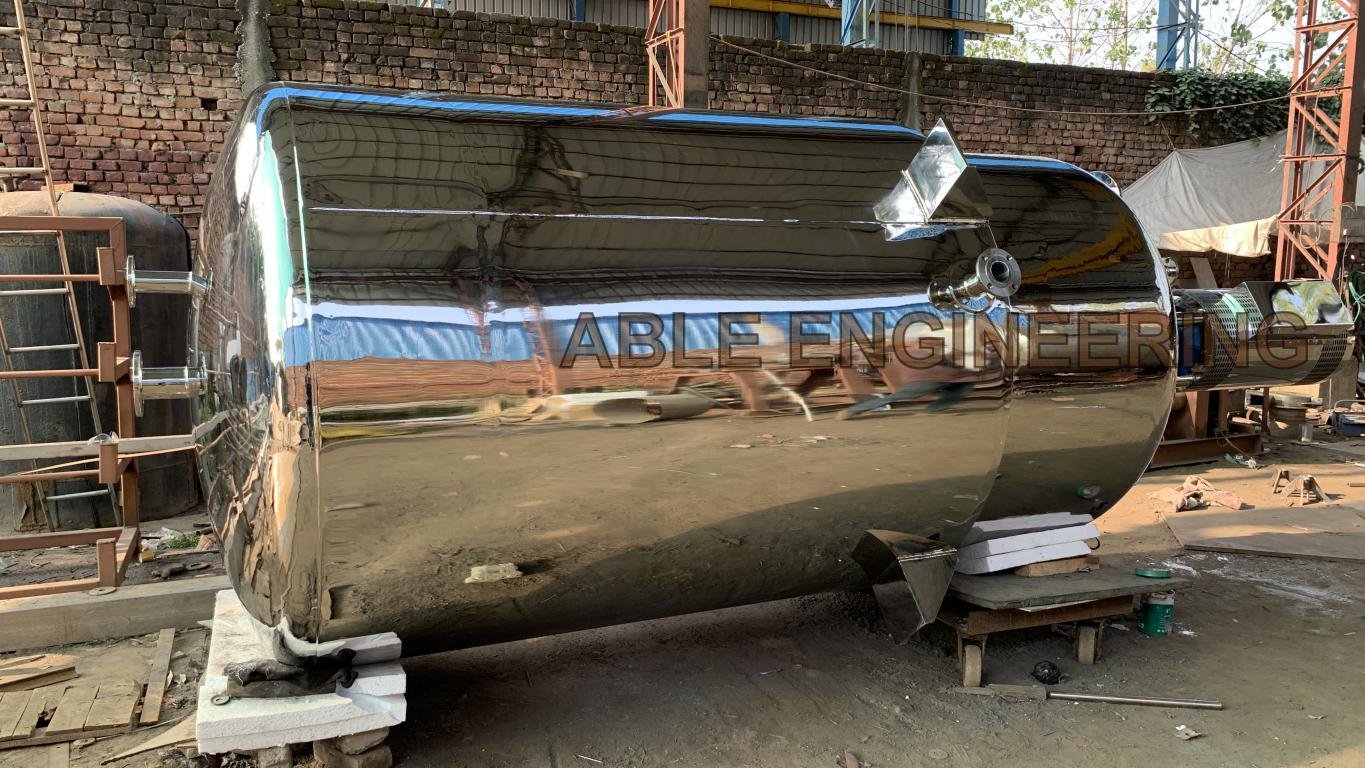
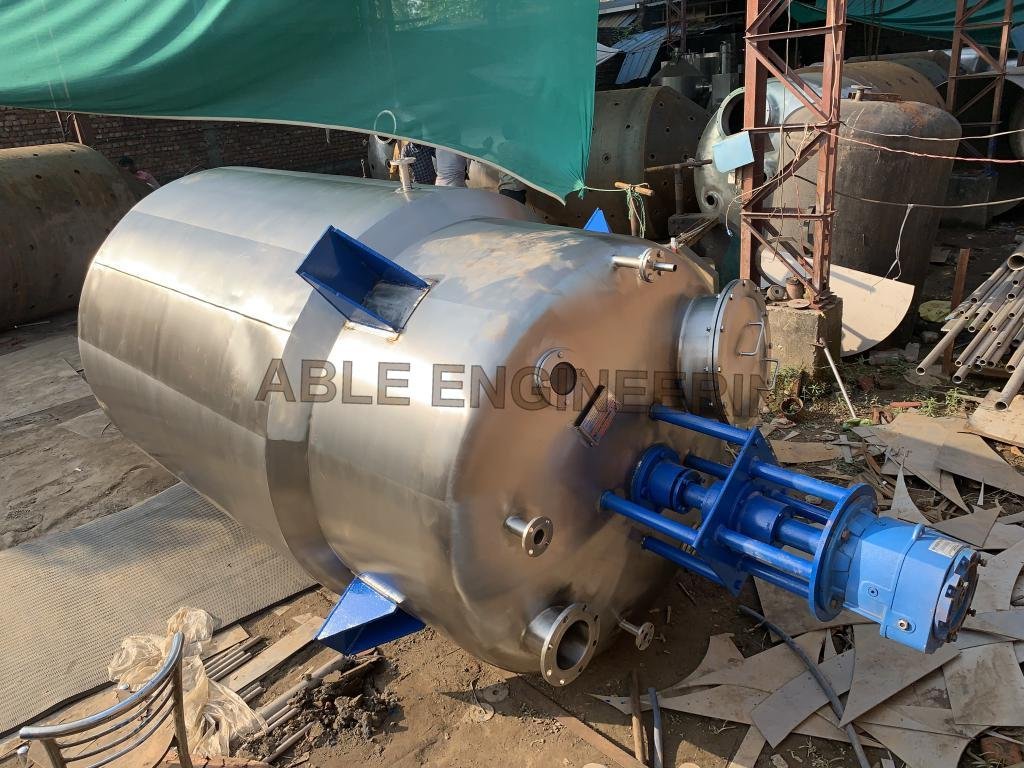
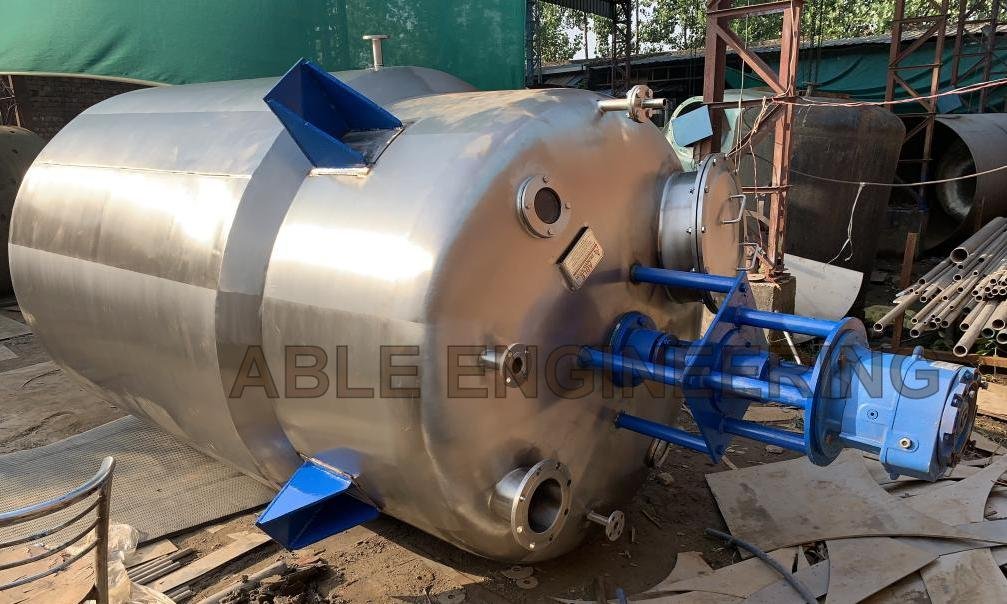
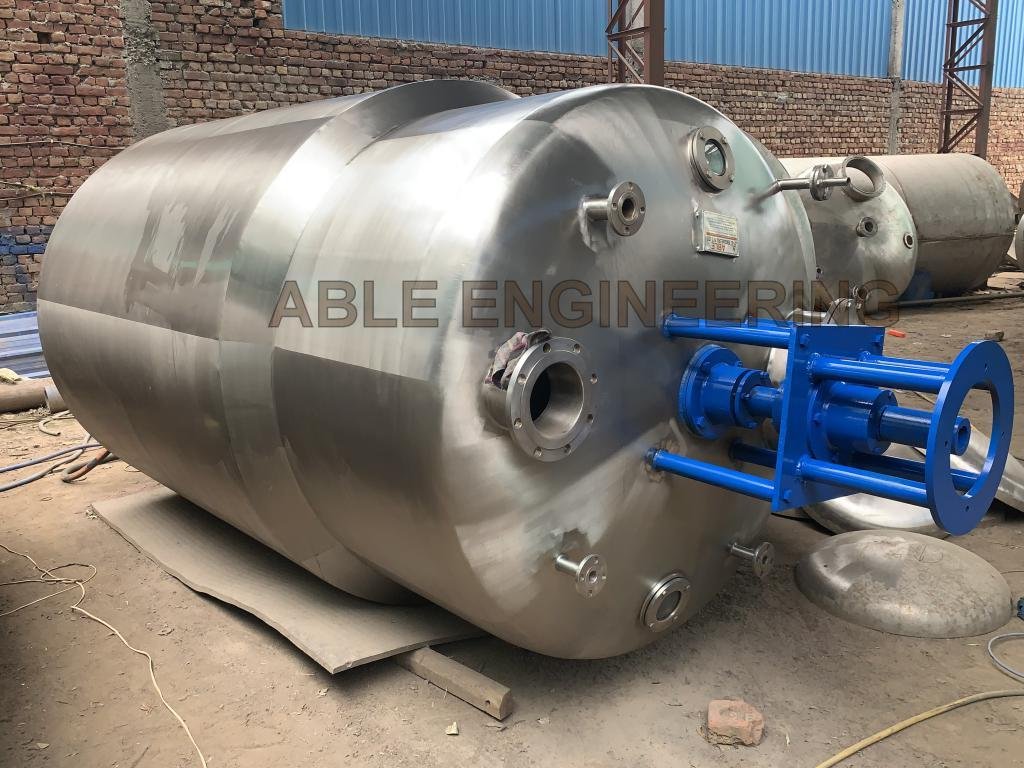
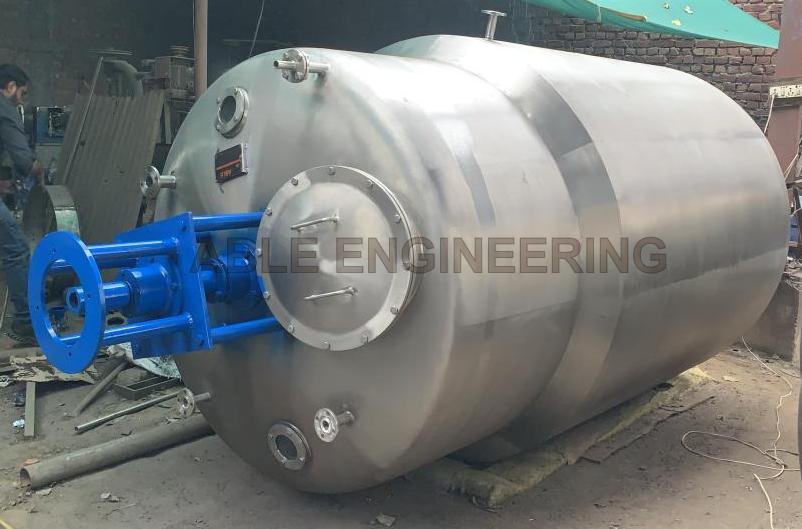
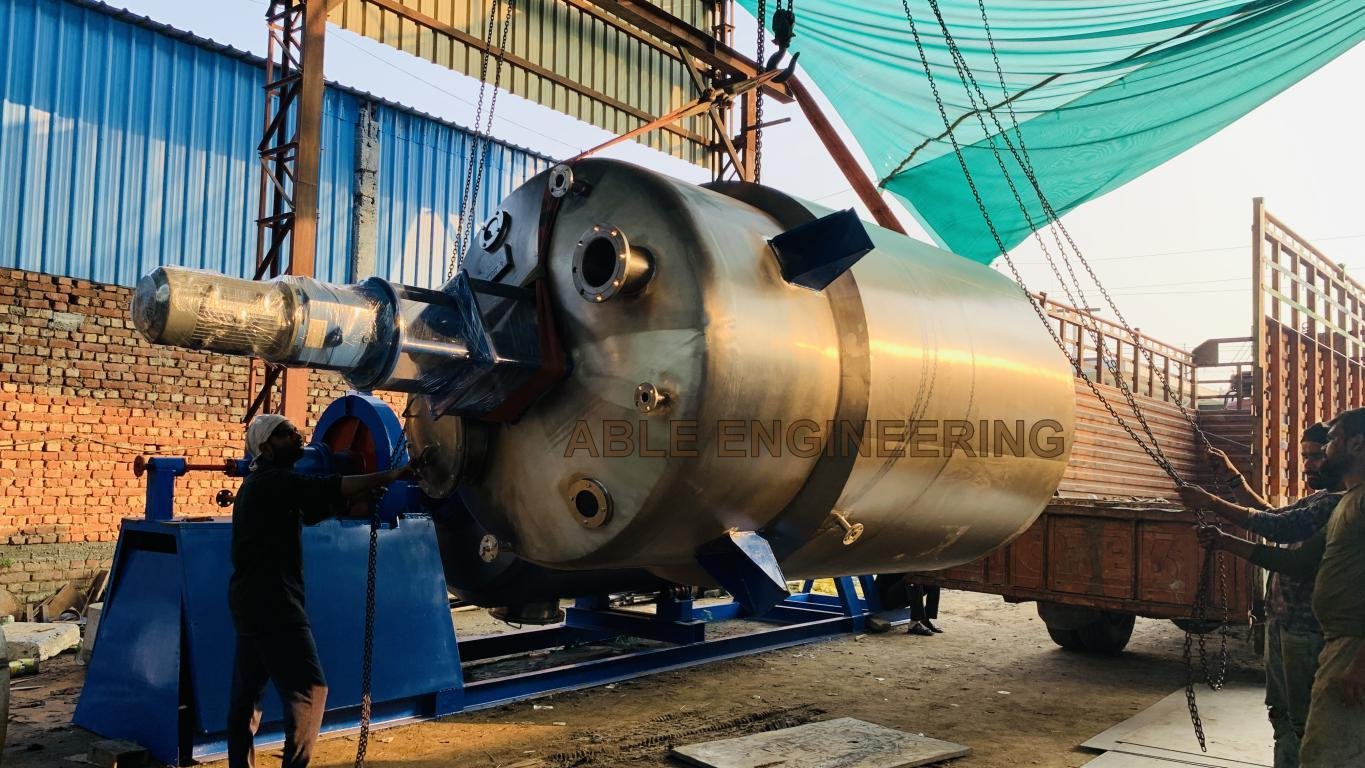
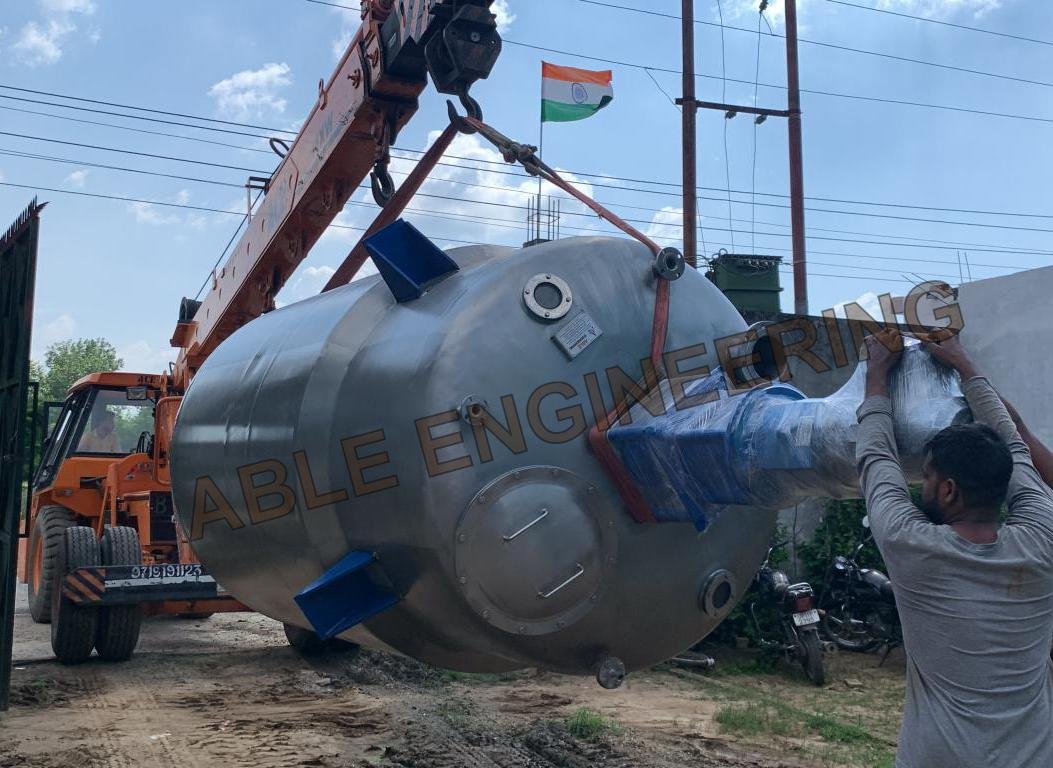
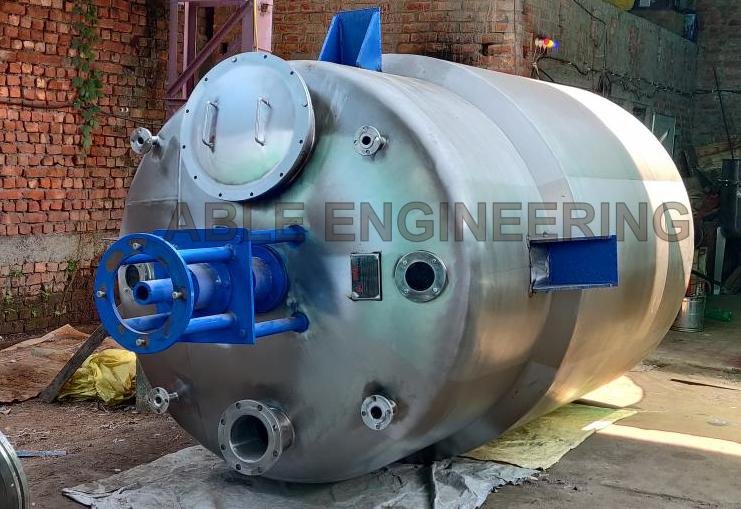
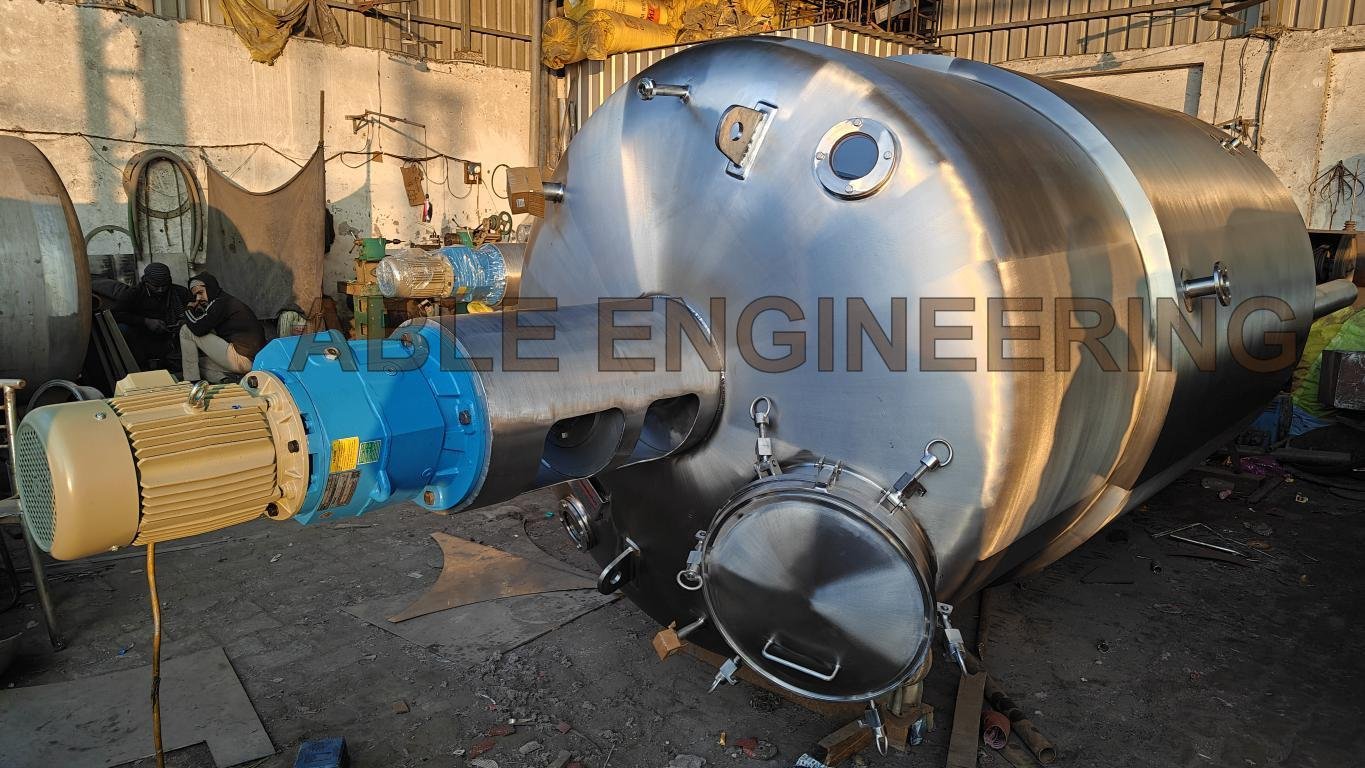
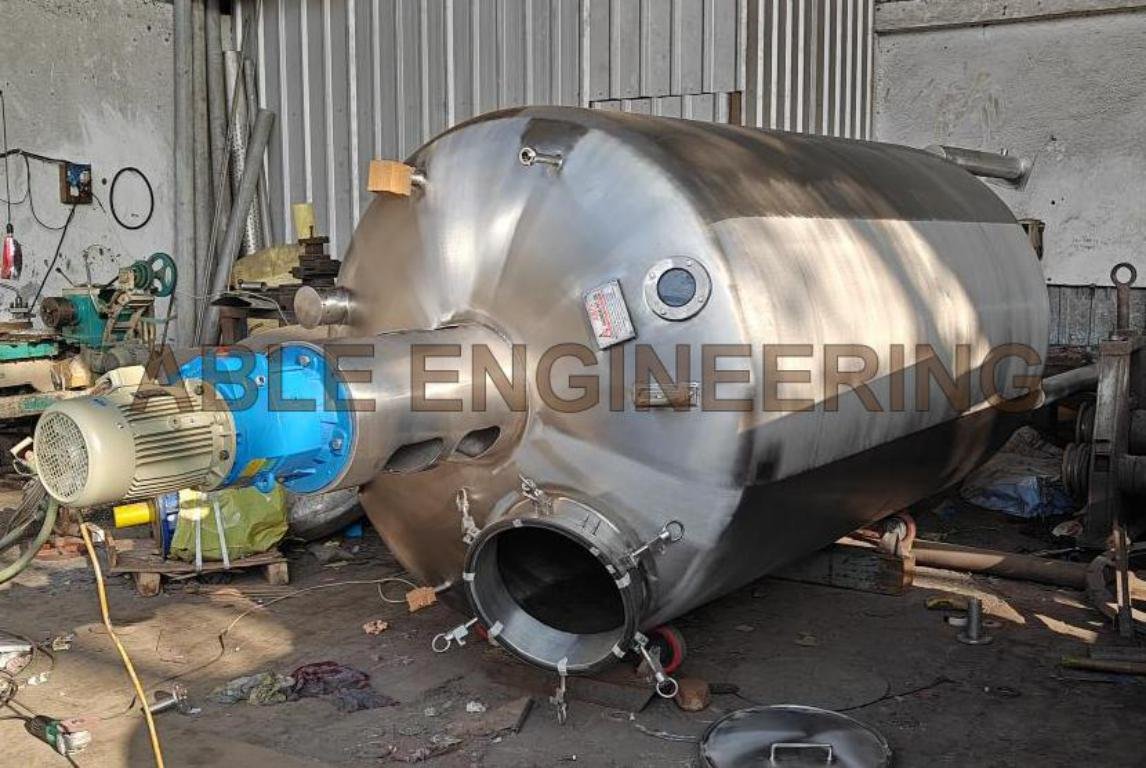
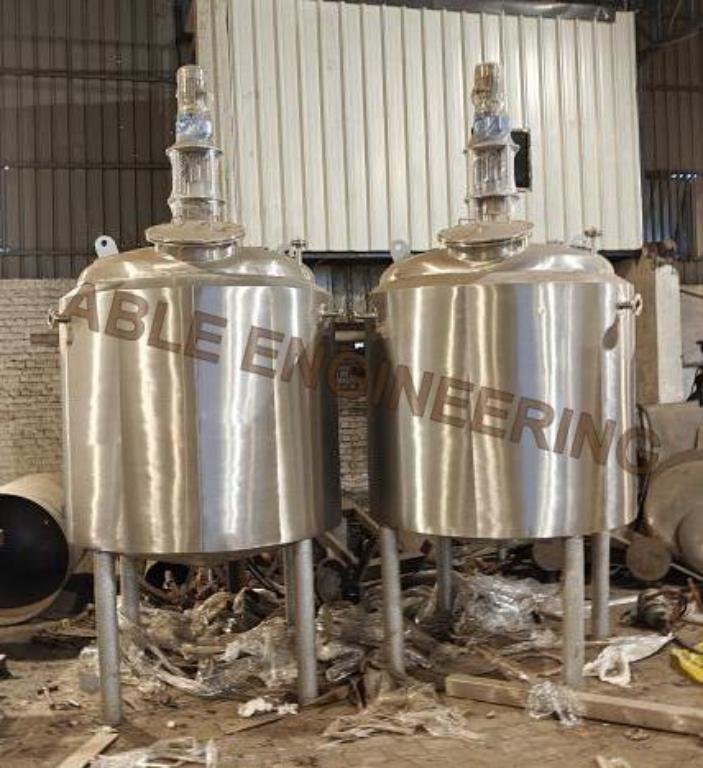
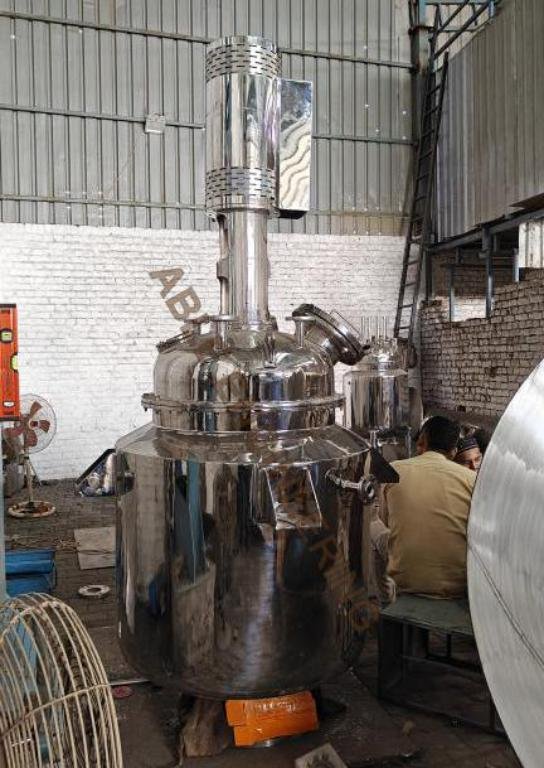
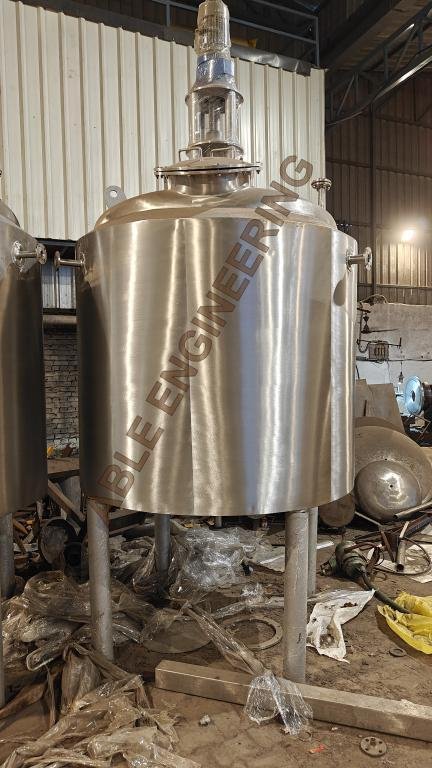
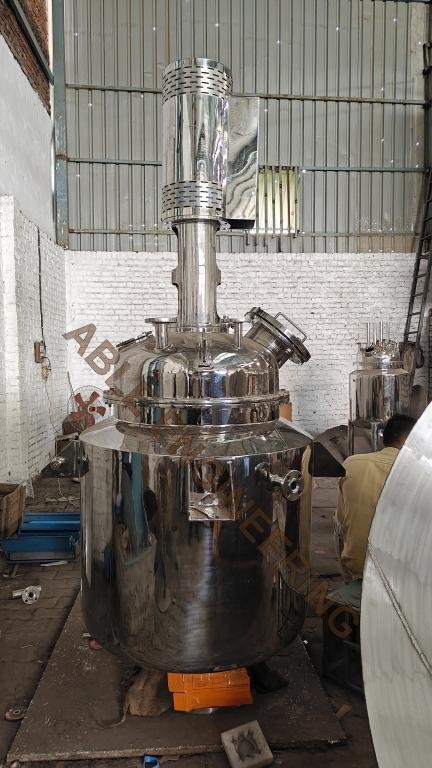
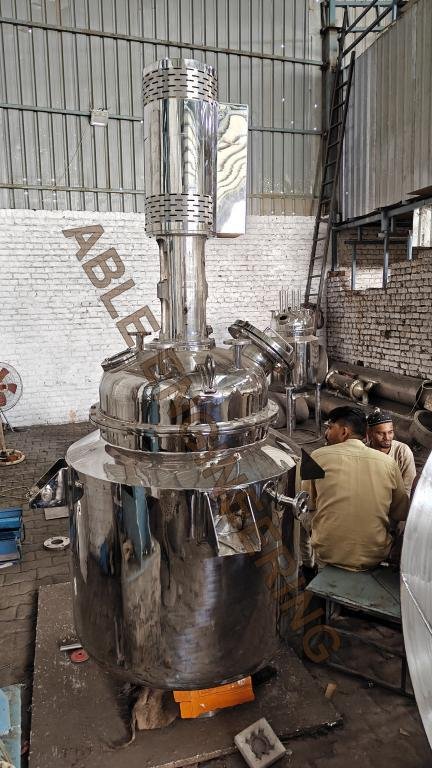
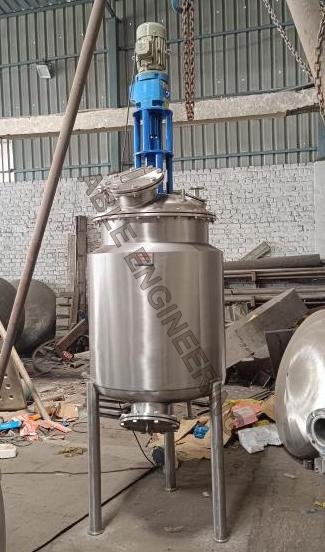
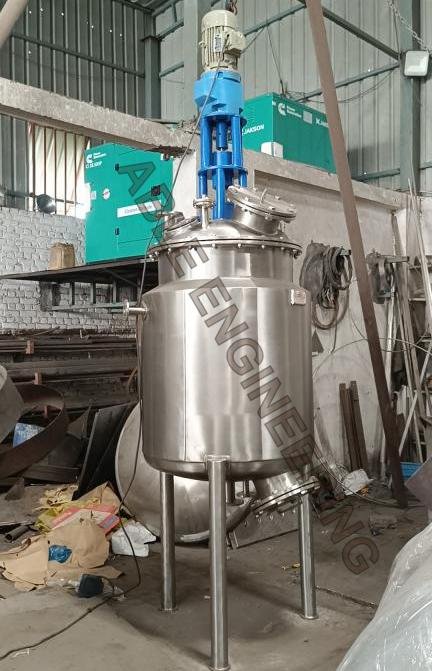
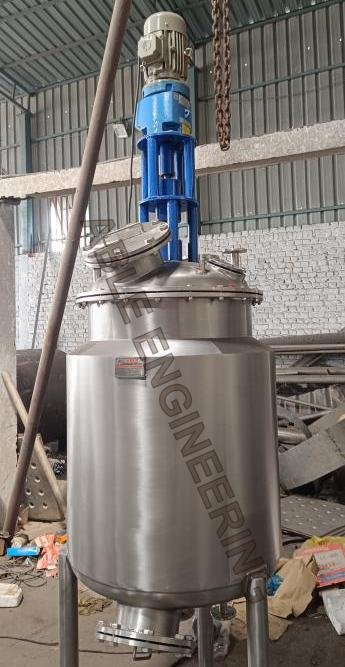
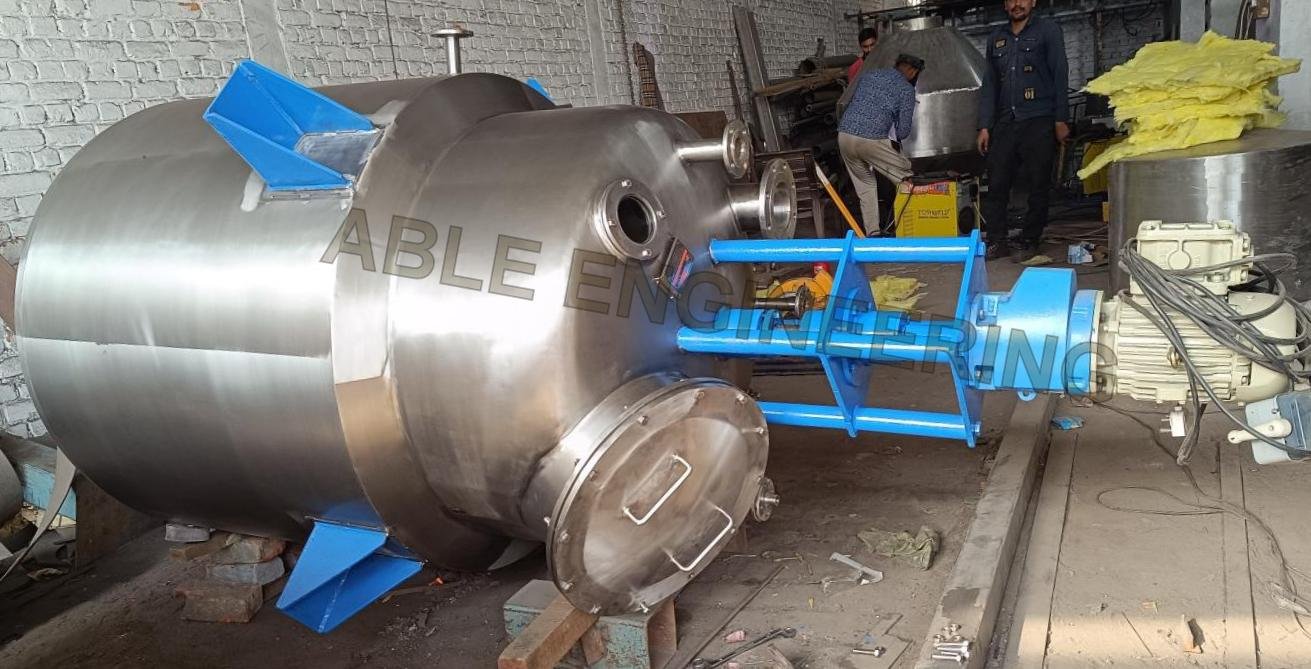
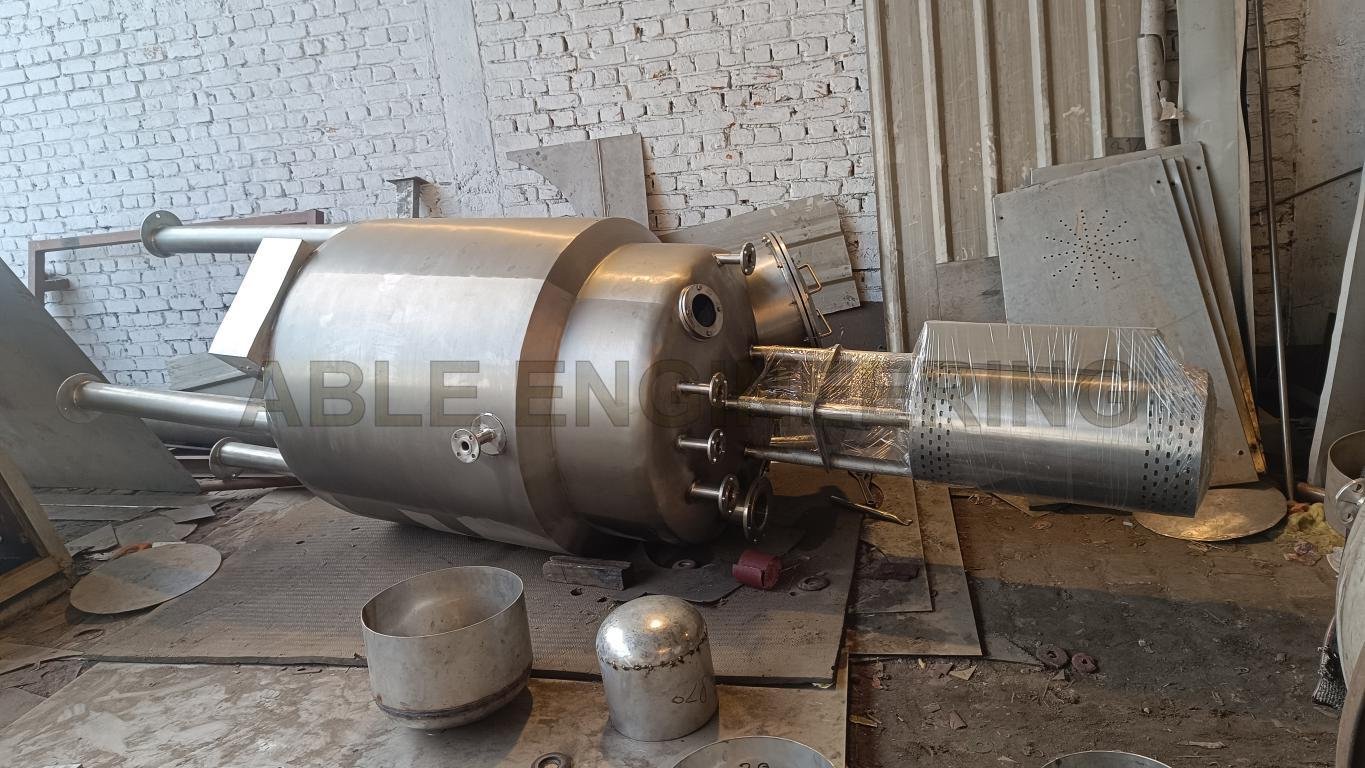
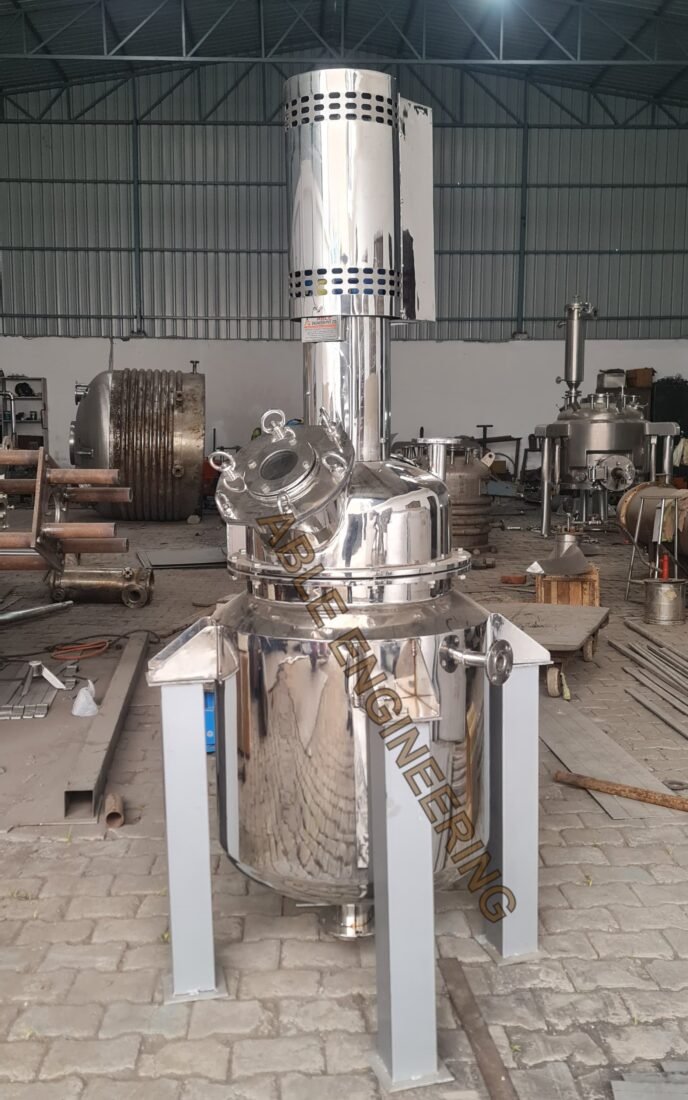
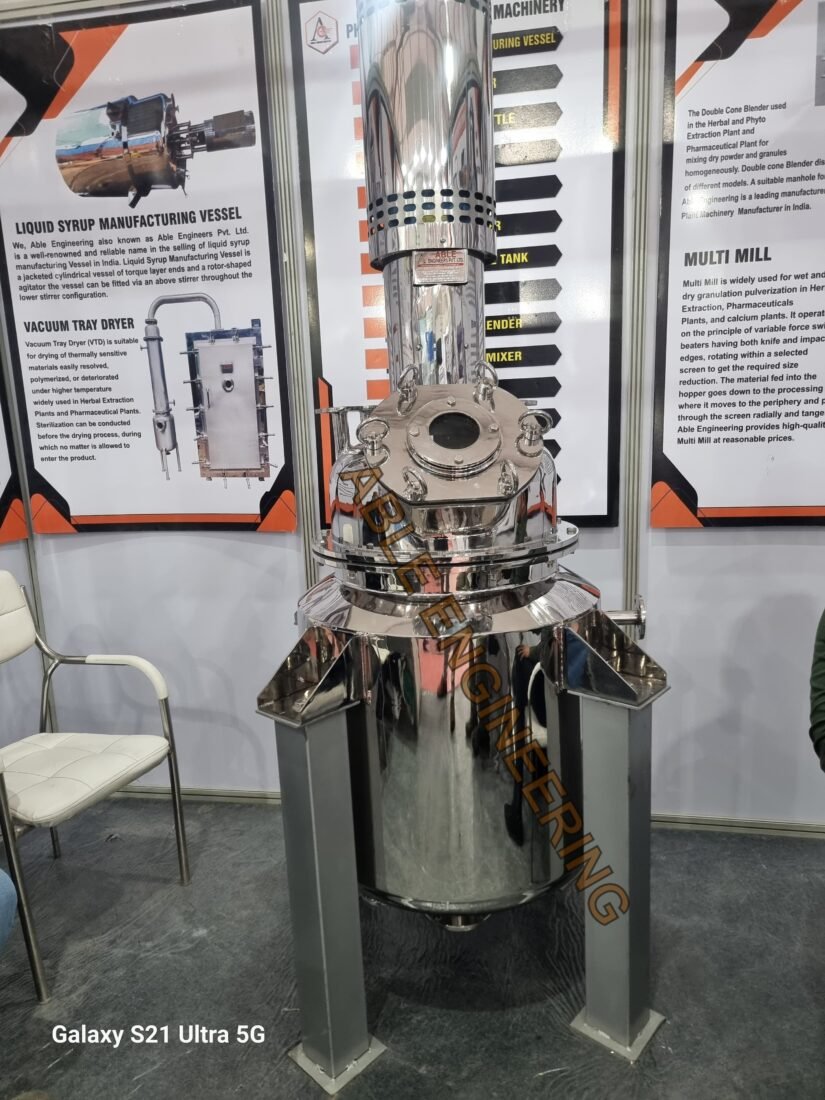
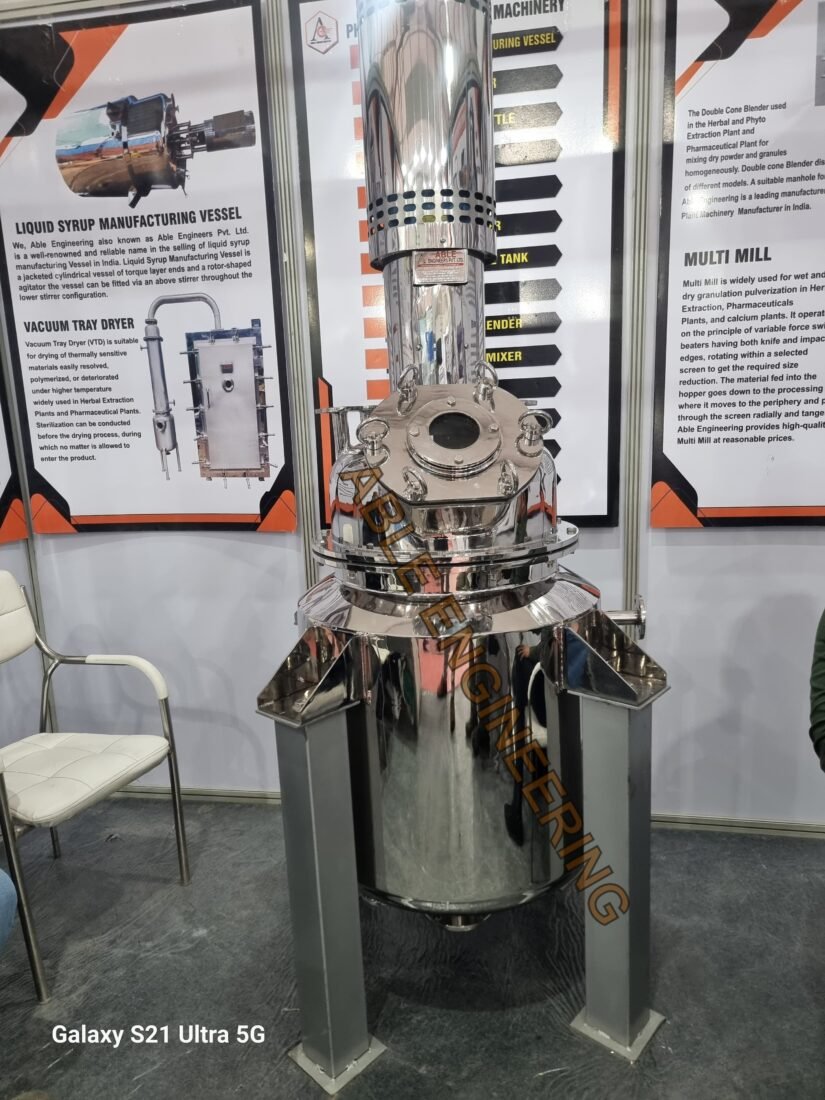
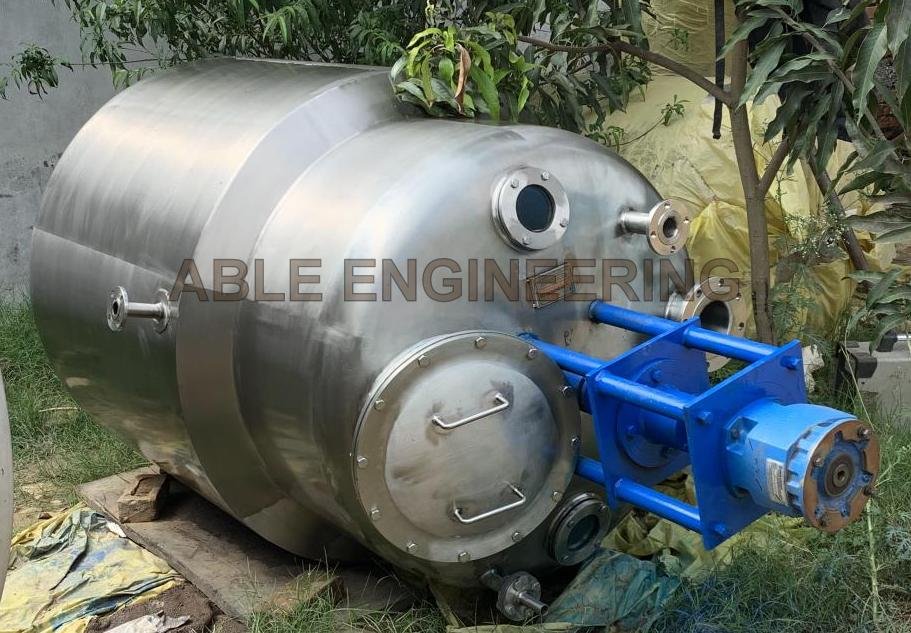
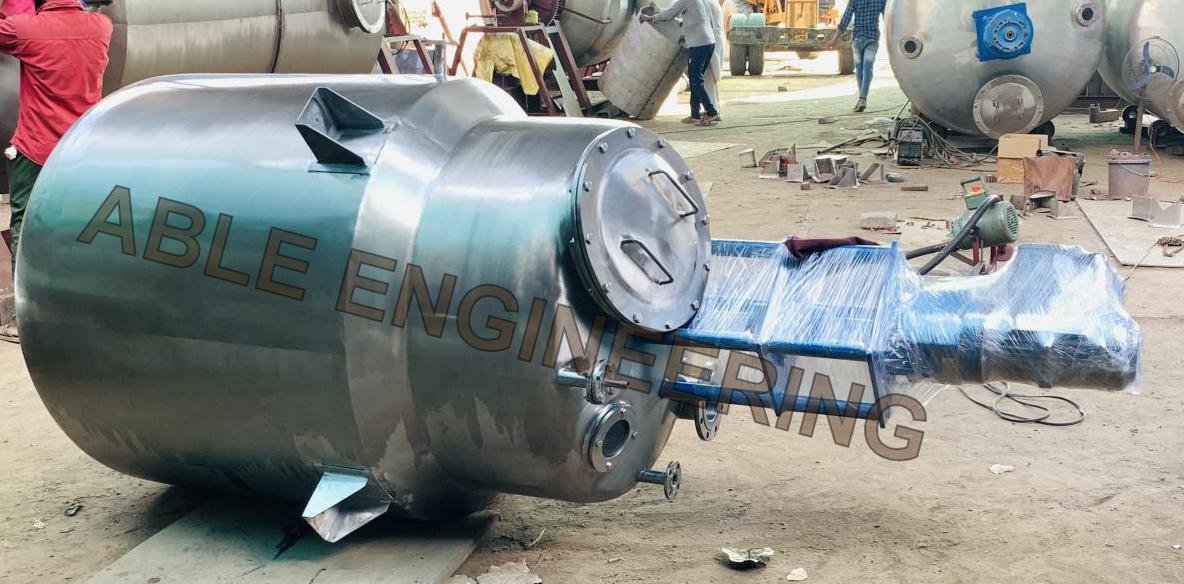
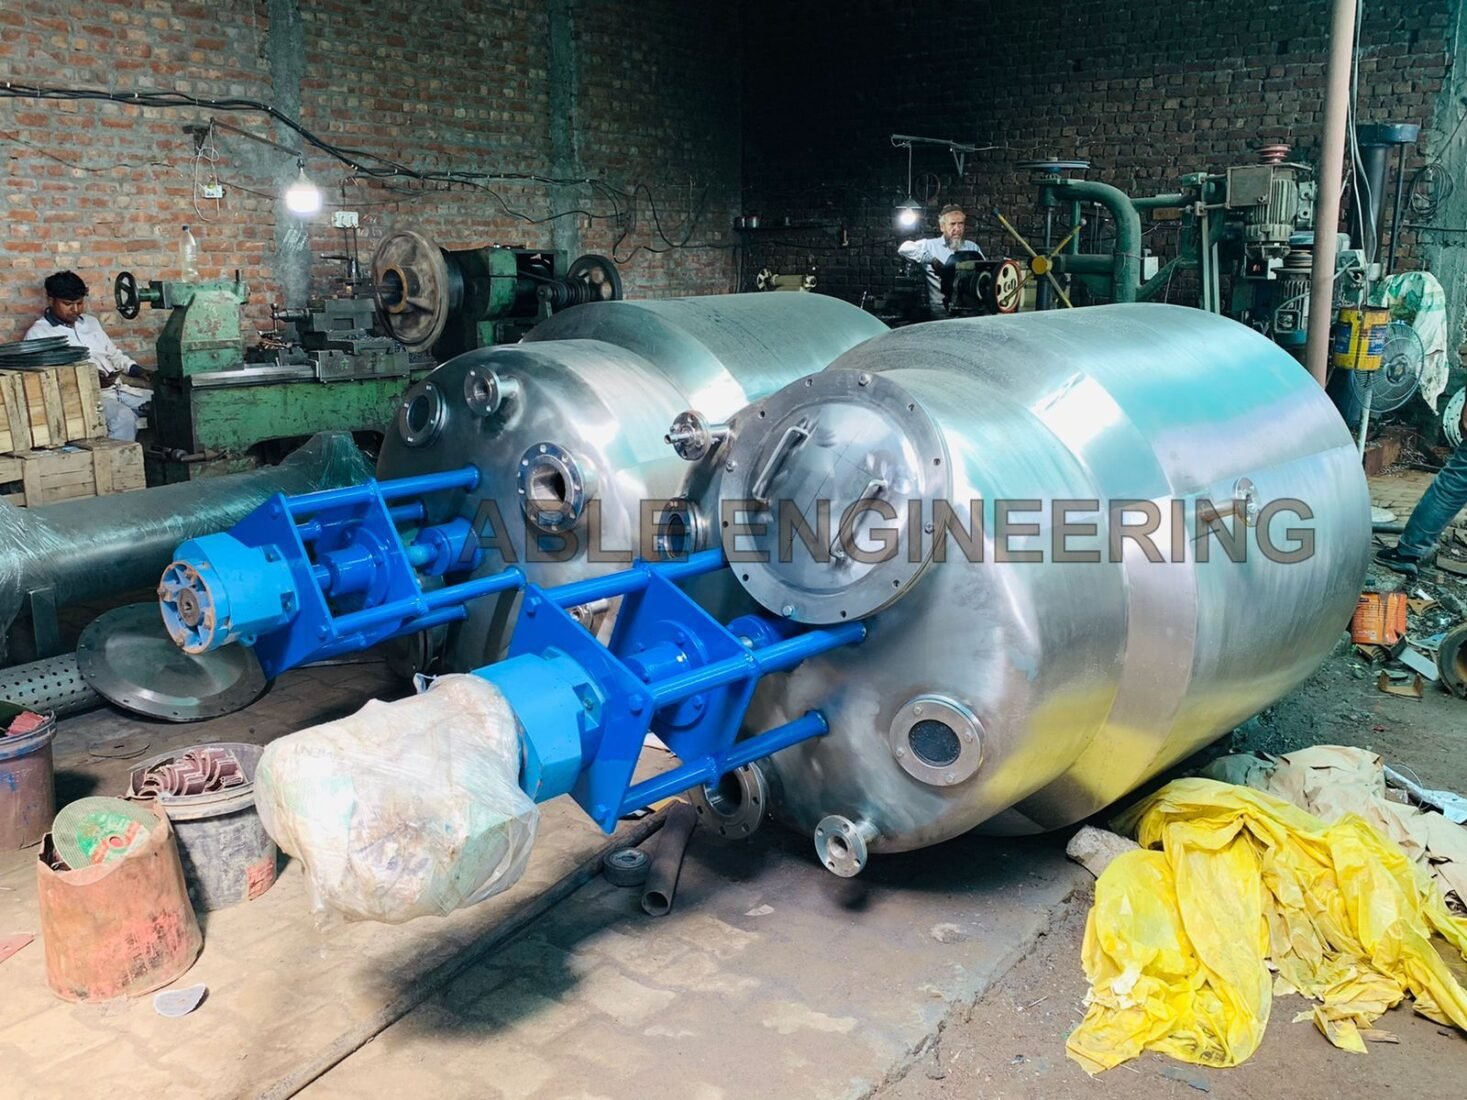
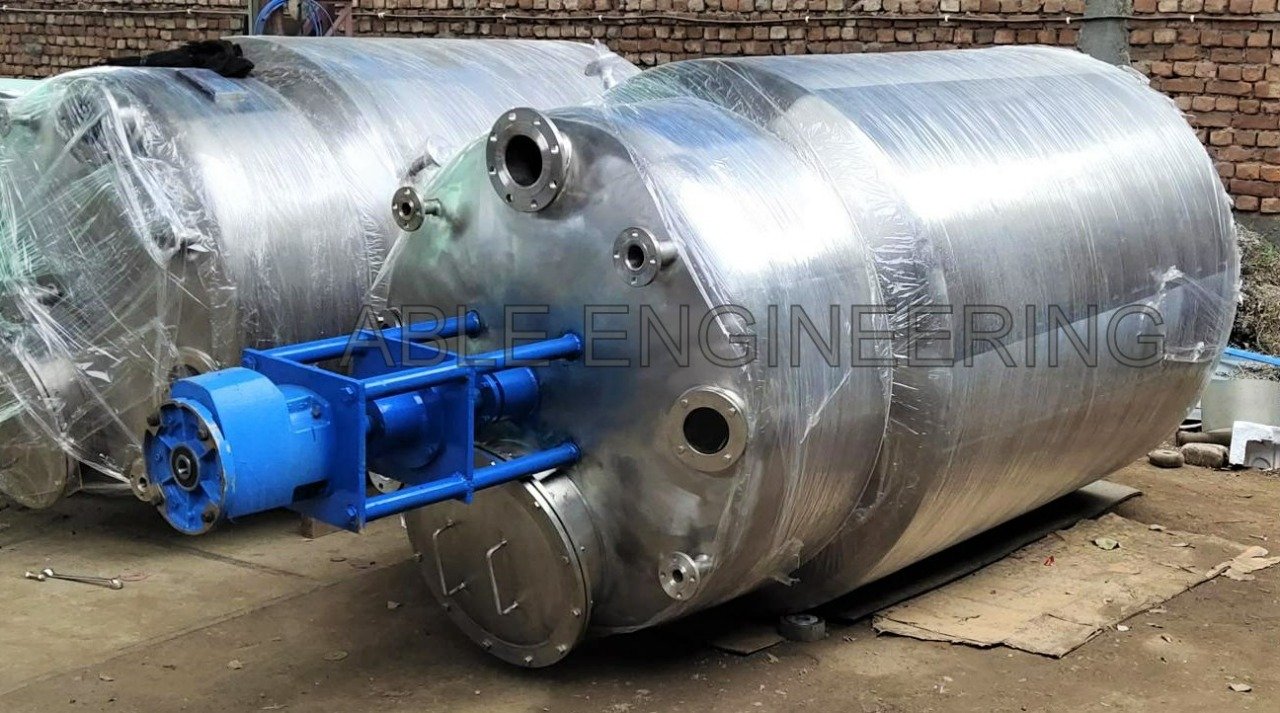
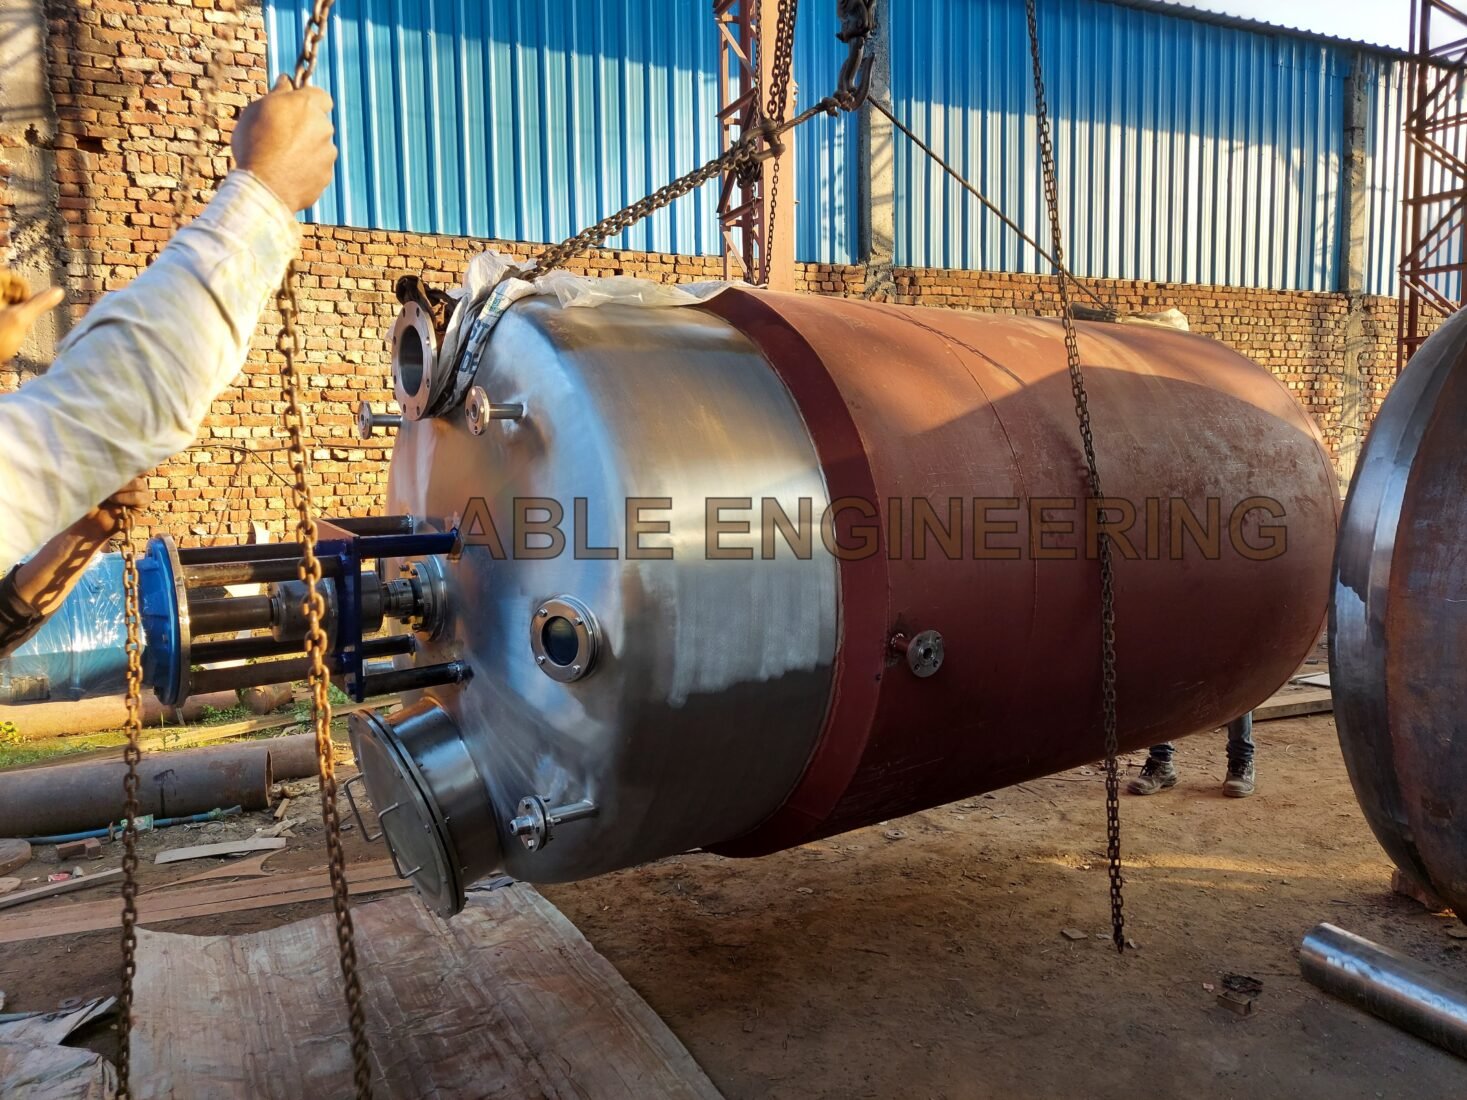
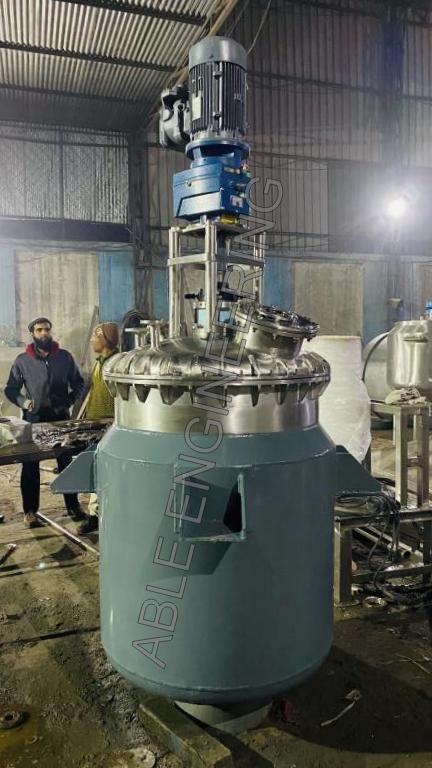
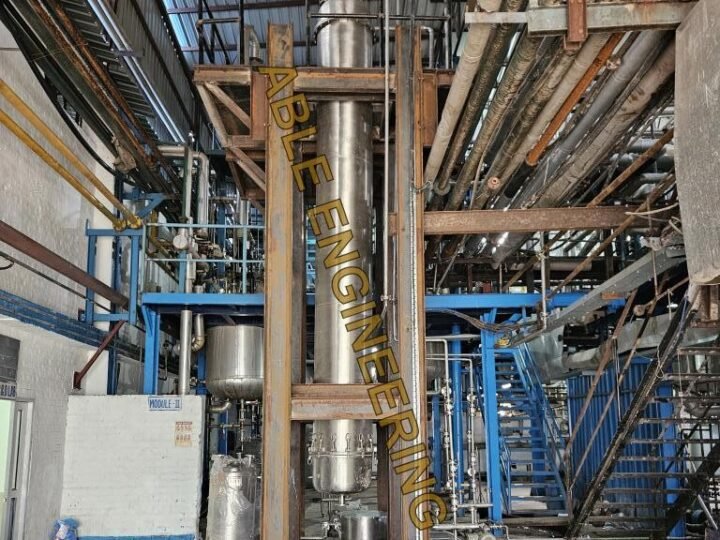
Chemical Reactor used in Herbal Extraction Plant, Pharmaceutical plants & chemical plants for any chemical changes and processes of reaction.

Built around your process.
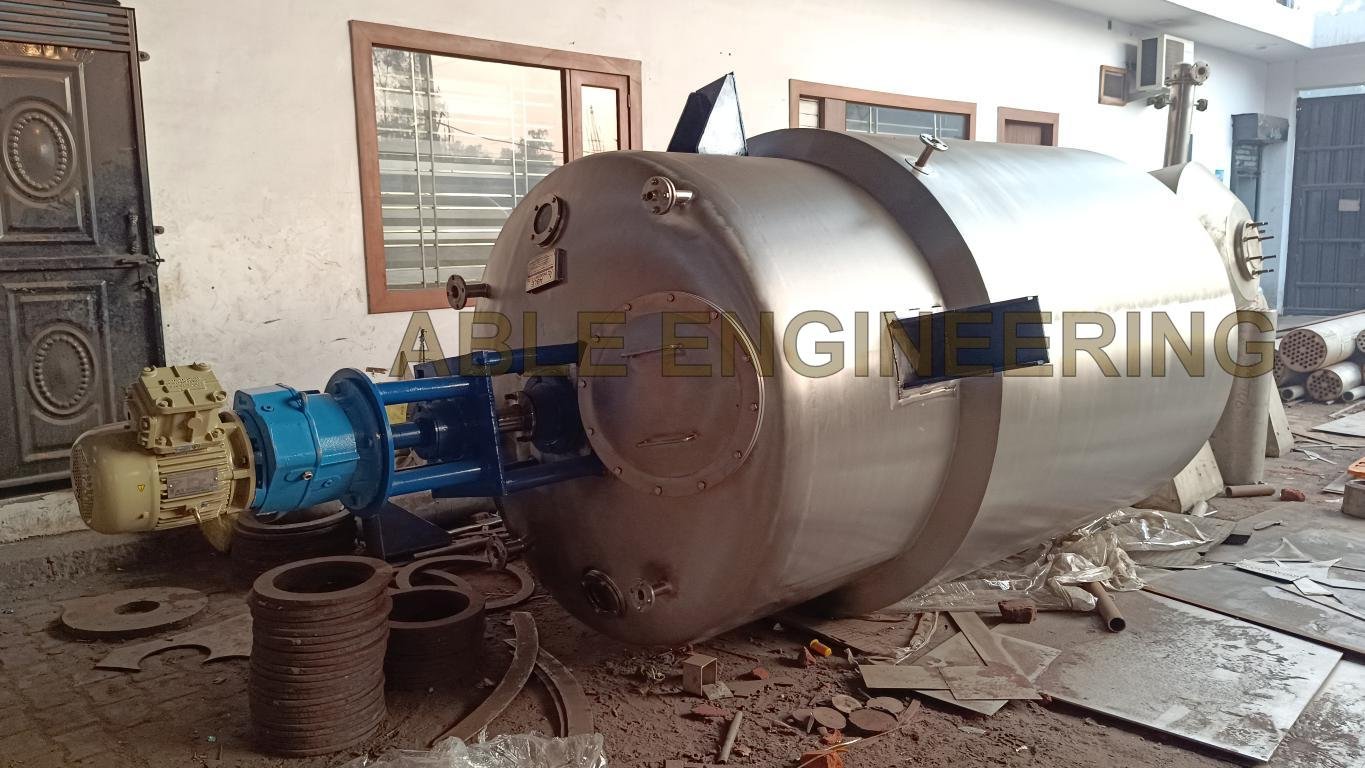
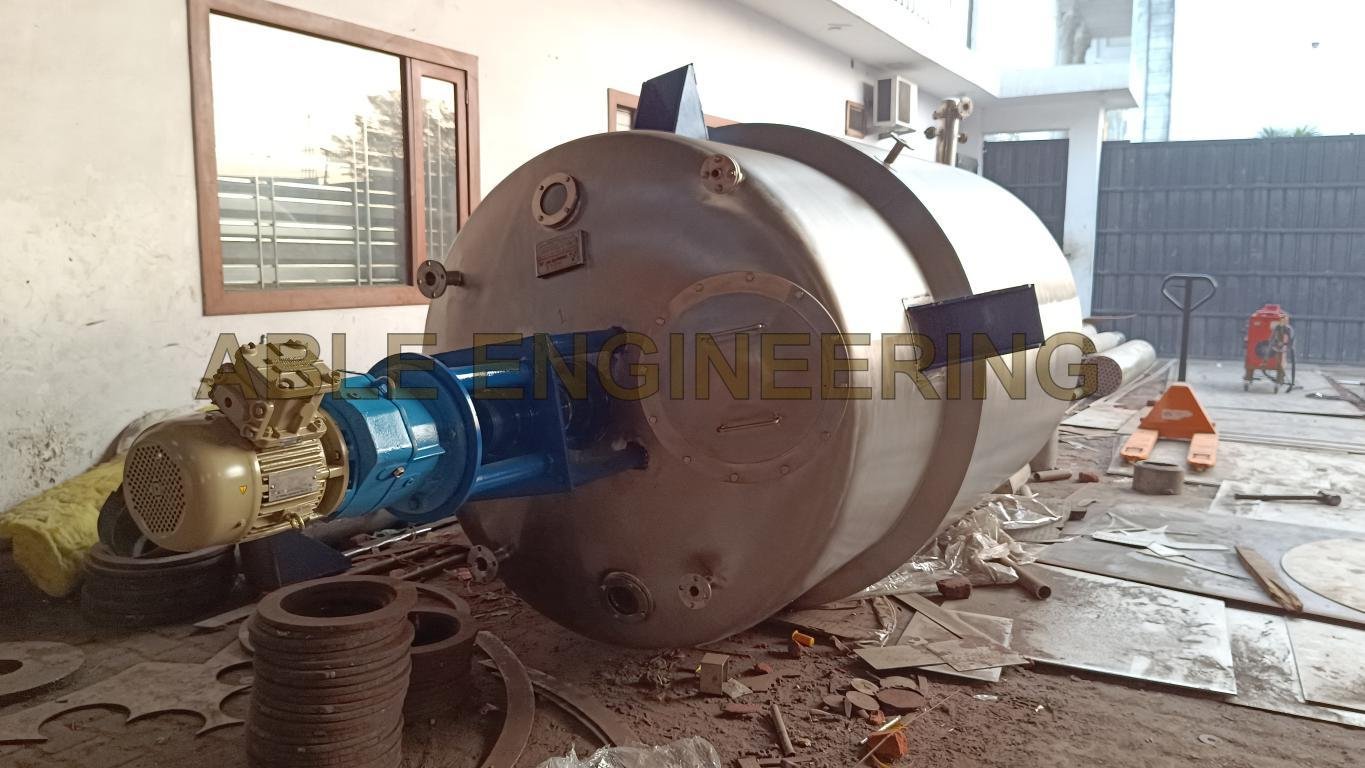
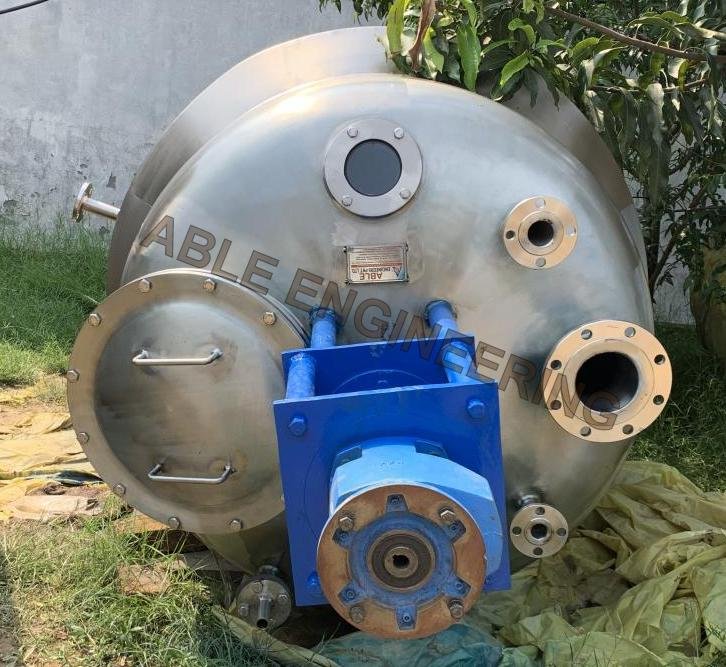
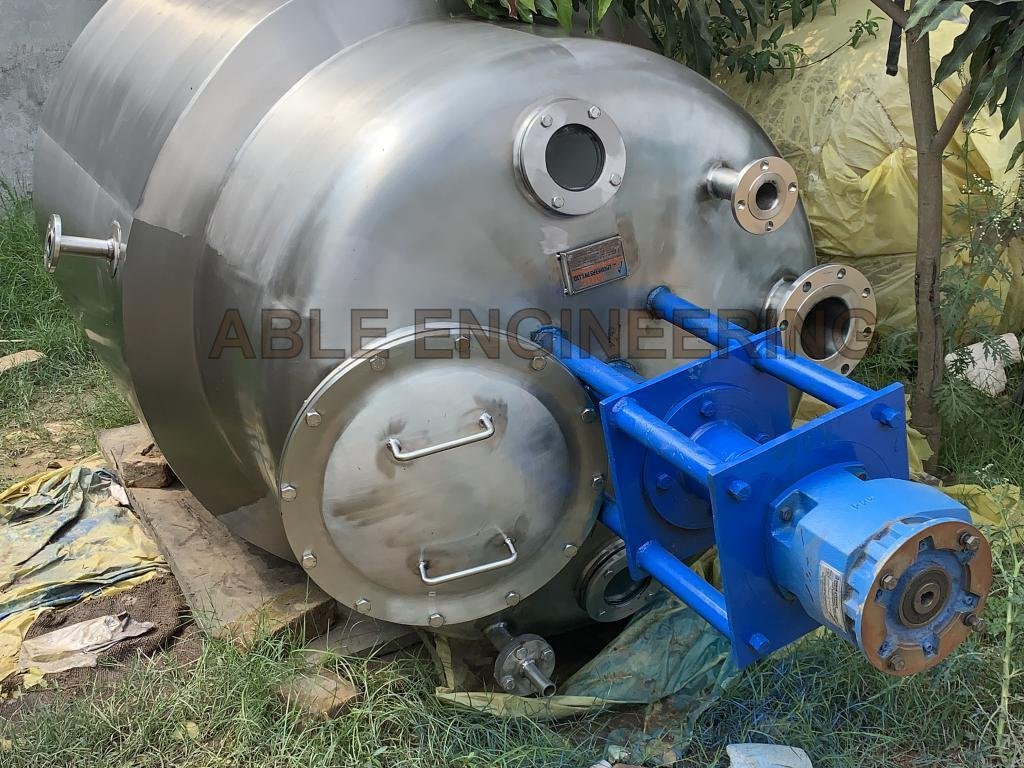
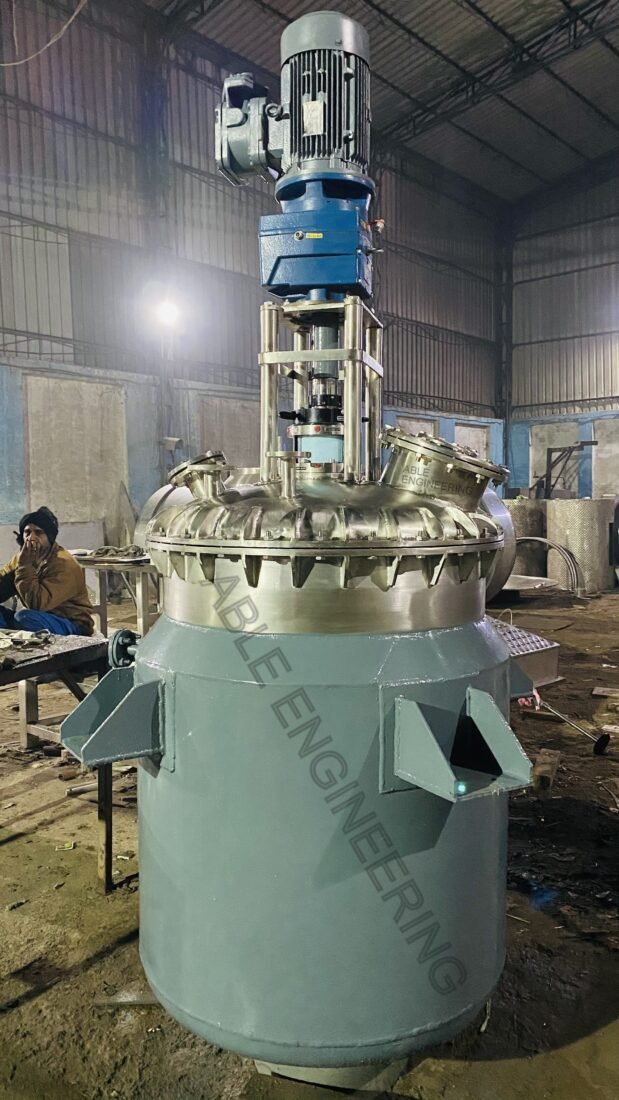
A Chemical Reactor is an industrial processing vessel used in Herbal Extraction Plants, Pharmaceutical Plants, and Chemical Plants to carry out chemical changes and various reaction processes. Chemical reactors form the core of chemical processing operations, where controlled conditions facilitate different types of chemical reactions.
Chemical Reactors are widely used for reactions such as condensation, polymerization, esterification, etherification, hydrolysis, hydration, reduction, oxidation, and hydrogenation. Manufacturers generally construct these reactors using stainless steel and provide different agitator arrangements according to process requirements.
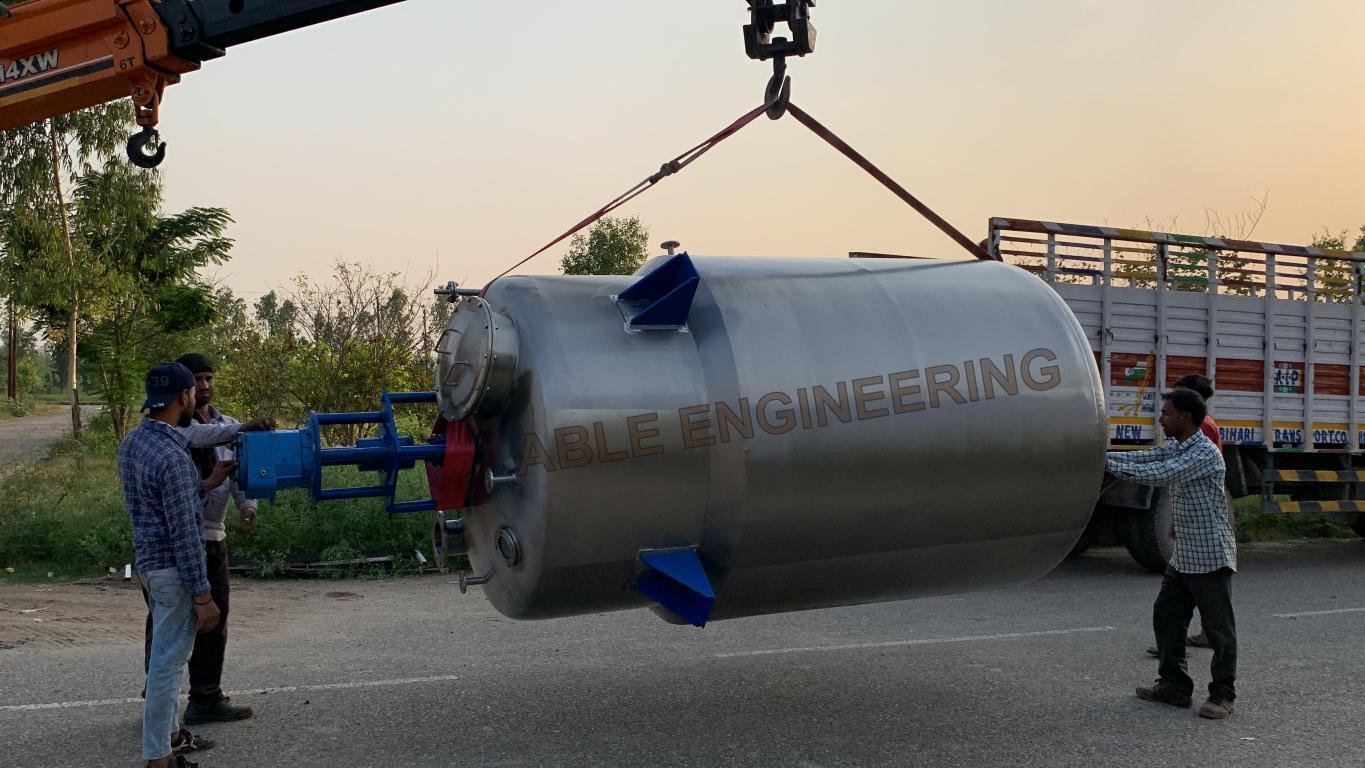
Able Engineers Private Limited manufactures Chemical Reactors in a wide range of capacities, from 500 litres to 25000 litres, according to client requirements. We design reactors with suitable construction materials, agitation systems, and configurations to meet specific industrial applications.
Features of Chemical Reactor
- Stainless steel construction for industrial processing applications
- Suitable for various chemical reaction processes
- Available with different agitator configurations
- Customizable capacity from 500 litres to 25000 litres
- Designed according to process and production requirements
- Efficient mixing and agitation for chemical processing
- Durable construction for reliable industrial operation
- Suitable for different operating conditions and applications
Applications of Chemical Reactor
Chemical Reactors are used across various industries for carrying out controlled chemical reactions and processing operations.
- Herbal Extraction Industry: Chemical processing and reactions involved in herbal extraction
- Pharmaceutical Industry: Preparation and processing of pharmaceutical compounds and formulations
- Chemical Industry: Condensation, polymerization, esterification, etherification, hydrolysis, hydration, reduction, oxidation, and hydrogenation
- Ayurvedic Industry: Processing and preparation of herbal and plant-based formulations
- Nutraceutical Industry: Chemical processing of suitable nutritional ingredients and formulations
Technical Specifications of Chemical Reactor
| Parameter | Specification |
|---|---|
| Equipment Name | Chemical Reactor |
| Equipment Type | Industrial Reaction Vessel |
| Capacity Range | 500 Litres to 25000 Litres |
| Material of Construction | Stainless Steel / As per requirement |
| Agitator Types | Anchor, Propeller, Paddle, Pitched-Blade Turbine |
| Mixing System | As per process requirements |
| Application | Chemical Reactions and Processing |
| Design | Customized as per client requirements |
Capacity, material of construction, agitator type, and other technical specifications can be customized according to process conditions and client requirements.
Advantages
- Versatile Reaction Processing: Suitable for a wide range of chemical reactions and industrial processes.
- Efficient Agitation: Different agitator designs support effective mixing according to material characteristics.
- Flexible Capacity: Available in a wide range of capacities for different production requirements.
- Customized Design: Reactor configuration can be tailored to specific process needs.
- Durable Construction: Stainless steel construction supports reliable industrial performance.
- Wide Industrial Applications: Suitable for chemical, pharmaceutical, herbal extraction, Ayurvedic, and nutraceutical industries.
Chemical Reactor Manufacturer in India
Able Engineers Private Limited is a manufacturer and supplier of Chemical Reactors in India, offering industrial reaction vessels for Herbal Extraction Plants, Pharmaceutical Plants, Chemical Plants, and various other processing industries.
We manufacture Chemical Reactors in different capacities and configurations, using suitable stainless steel construction and agitator arrangements. Furthermore, we customize equipment according to client requirements, process conditions, and production capacity.
Contact Able Engineers Private Limited for customized Chemical Reactor solutions and Industrial Processing Equipment.
- Jacketed for steam or thermic-fluid heating
- Suitable for water, hydro-alcoholic and solvent extraction
- Charging manhole and quick discharge of spent herb
- Contact parts in SS 304 / SS 316 / SS 316L
- Built to cGMP with mirror or matt finish